Featured Titanium Hardware & Complementary CNC Components
Directly supporting high-stress automotive, chassis, and exhaust assemblies throughout Liechtenstein and neighboring Swiss-Austrian high-tech corridors with verified ASTM, DIN, and ISO compliance.
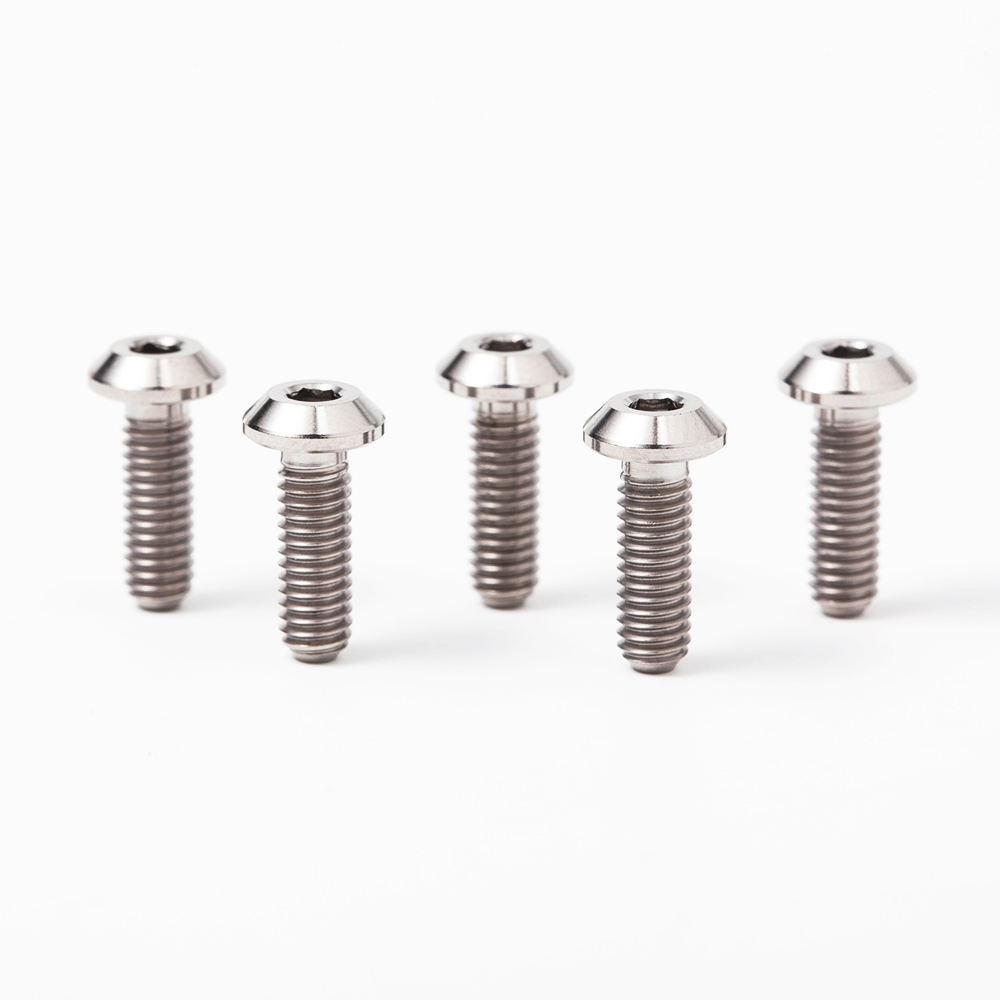
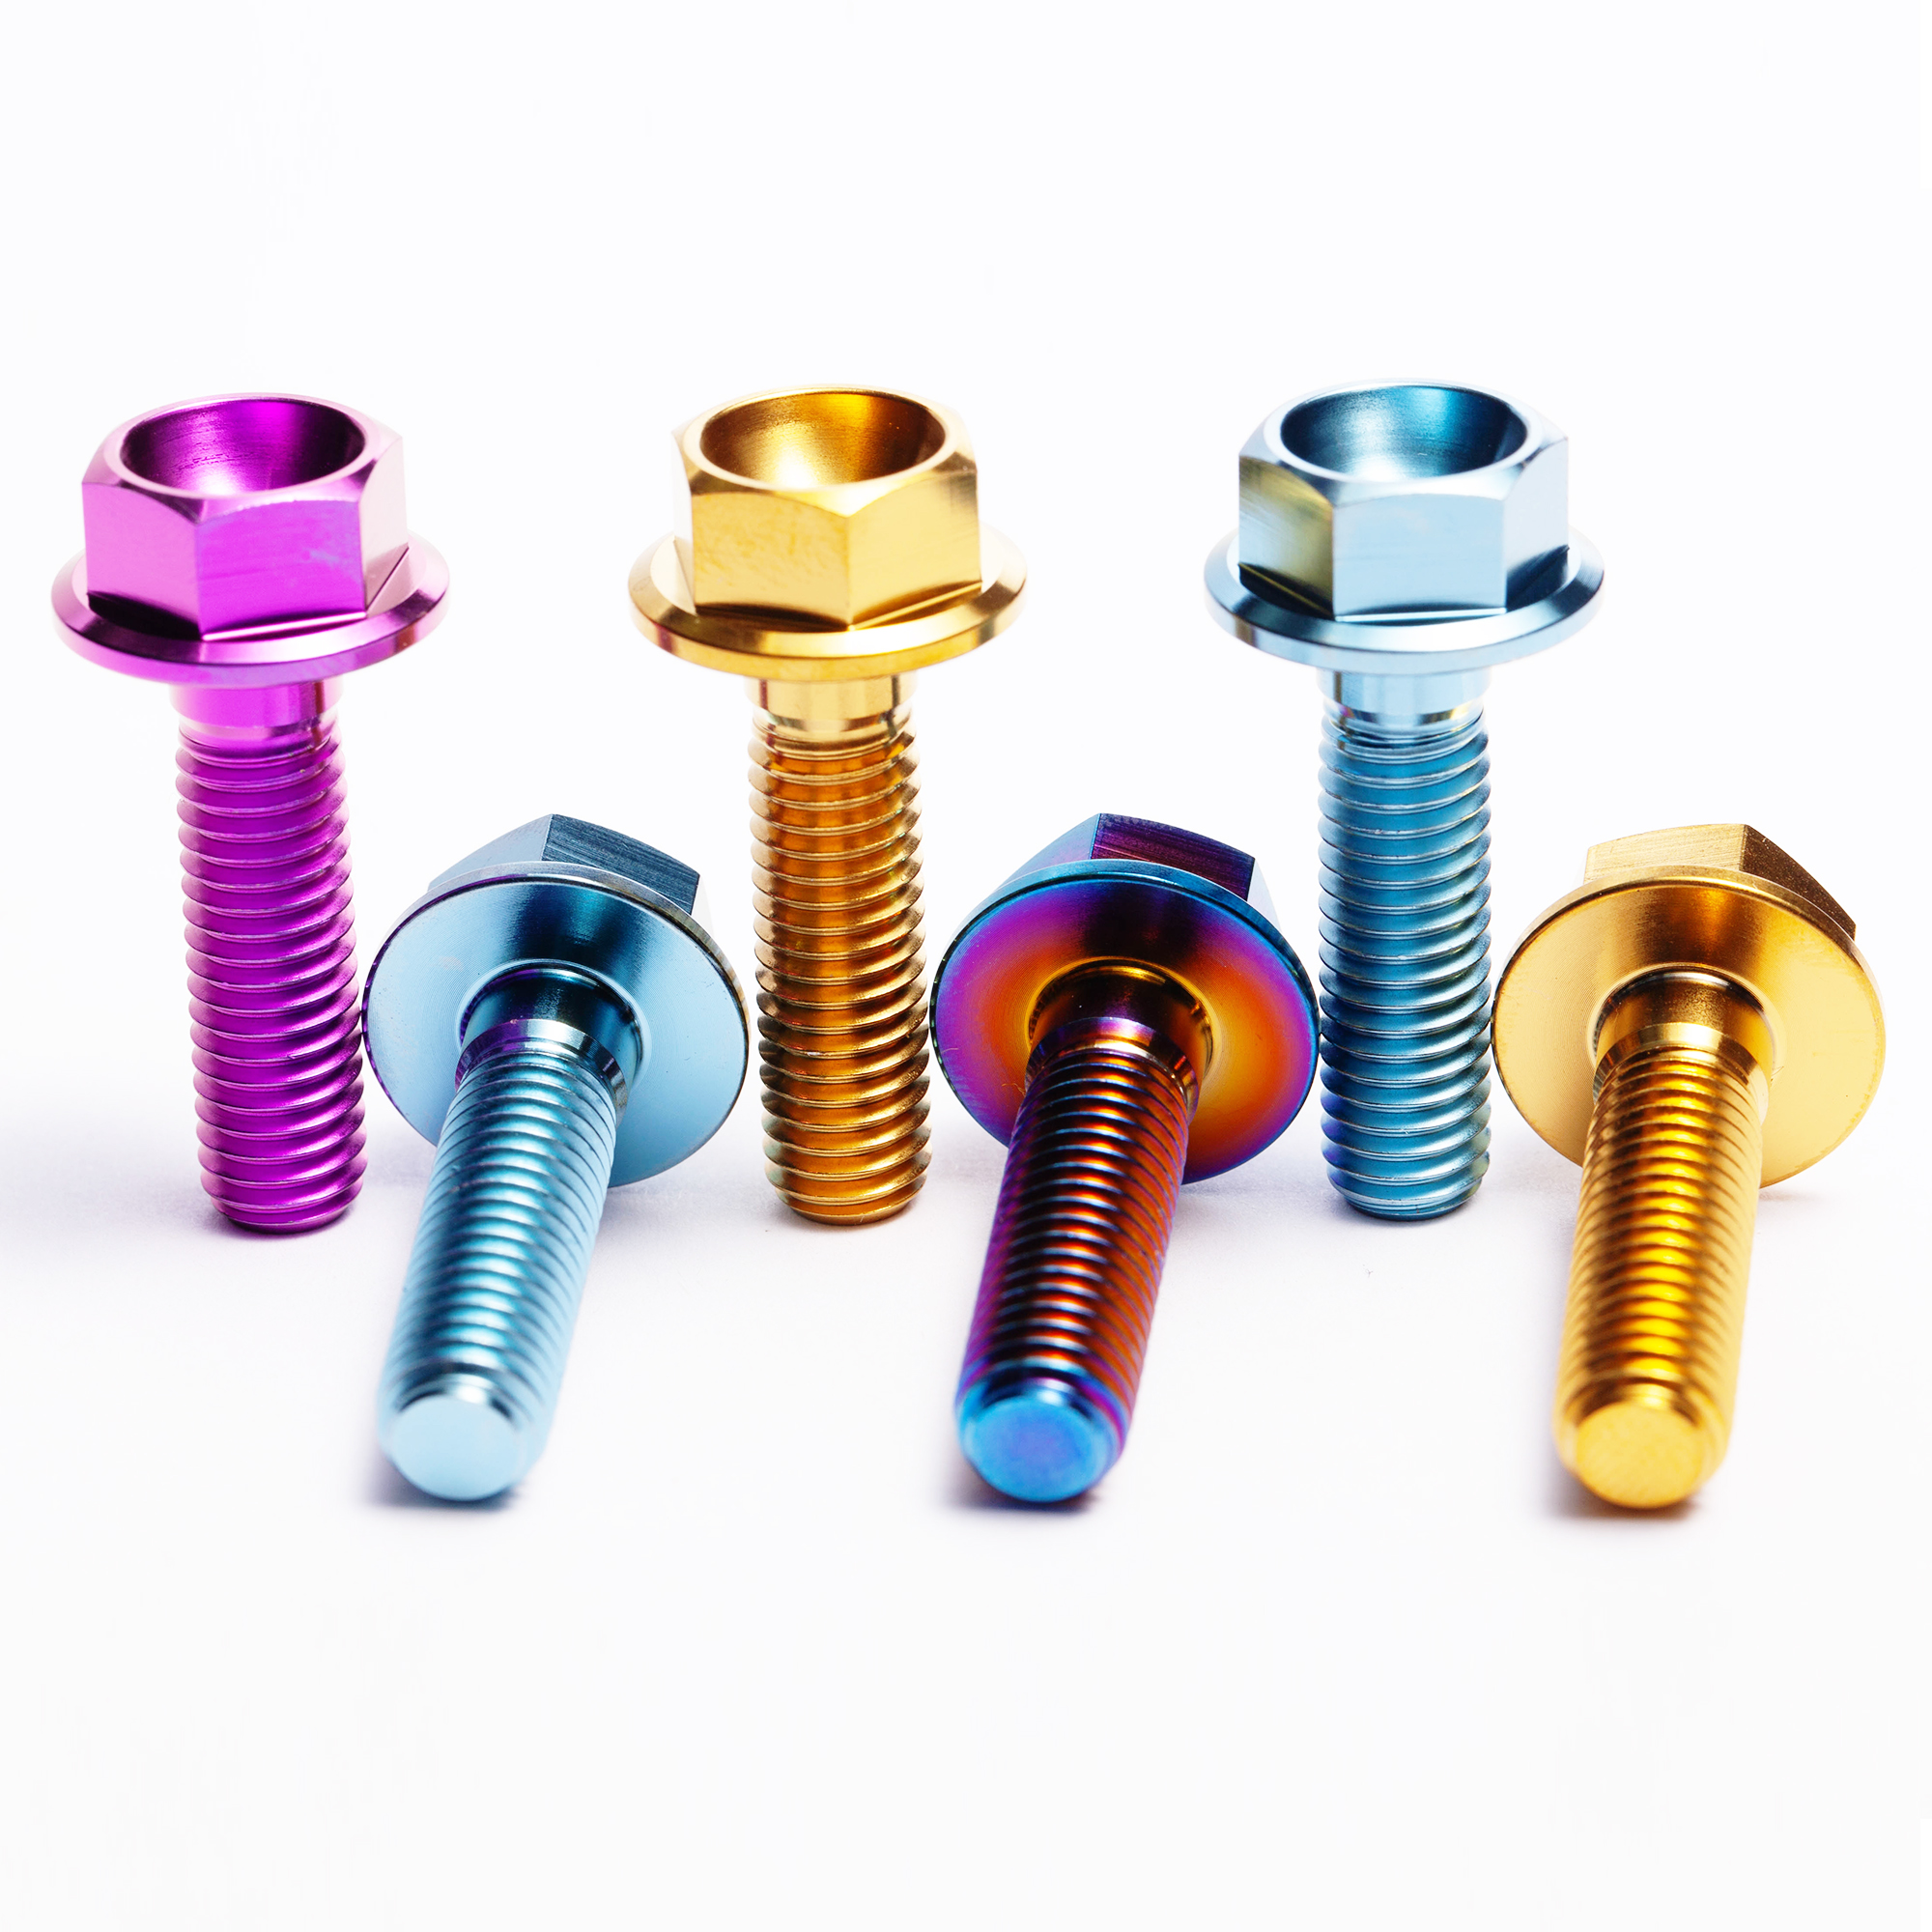
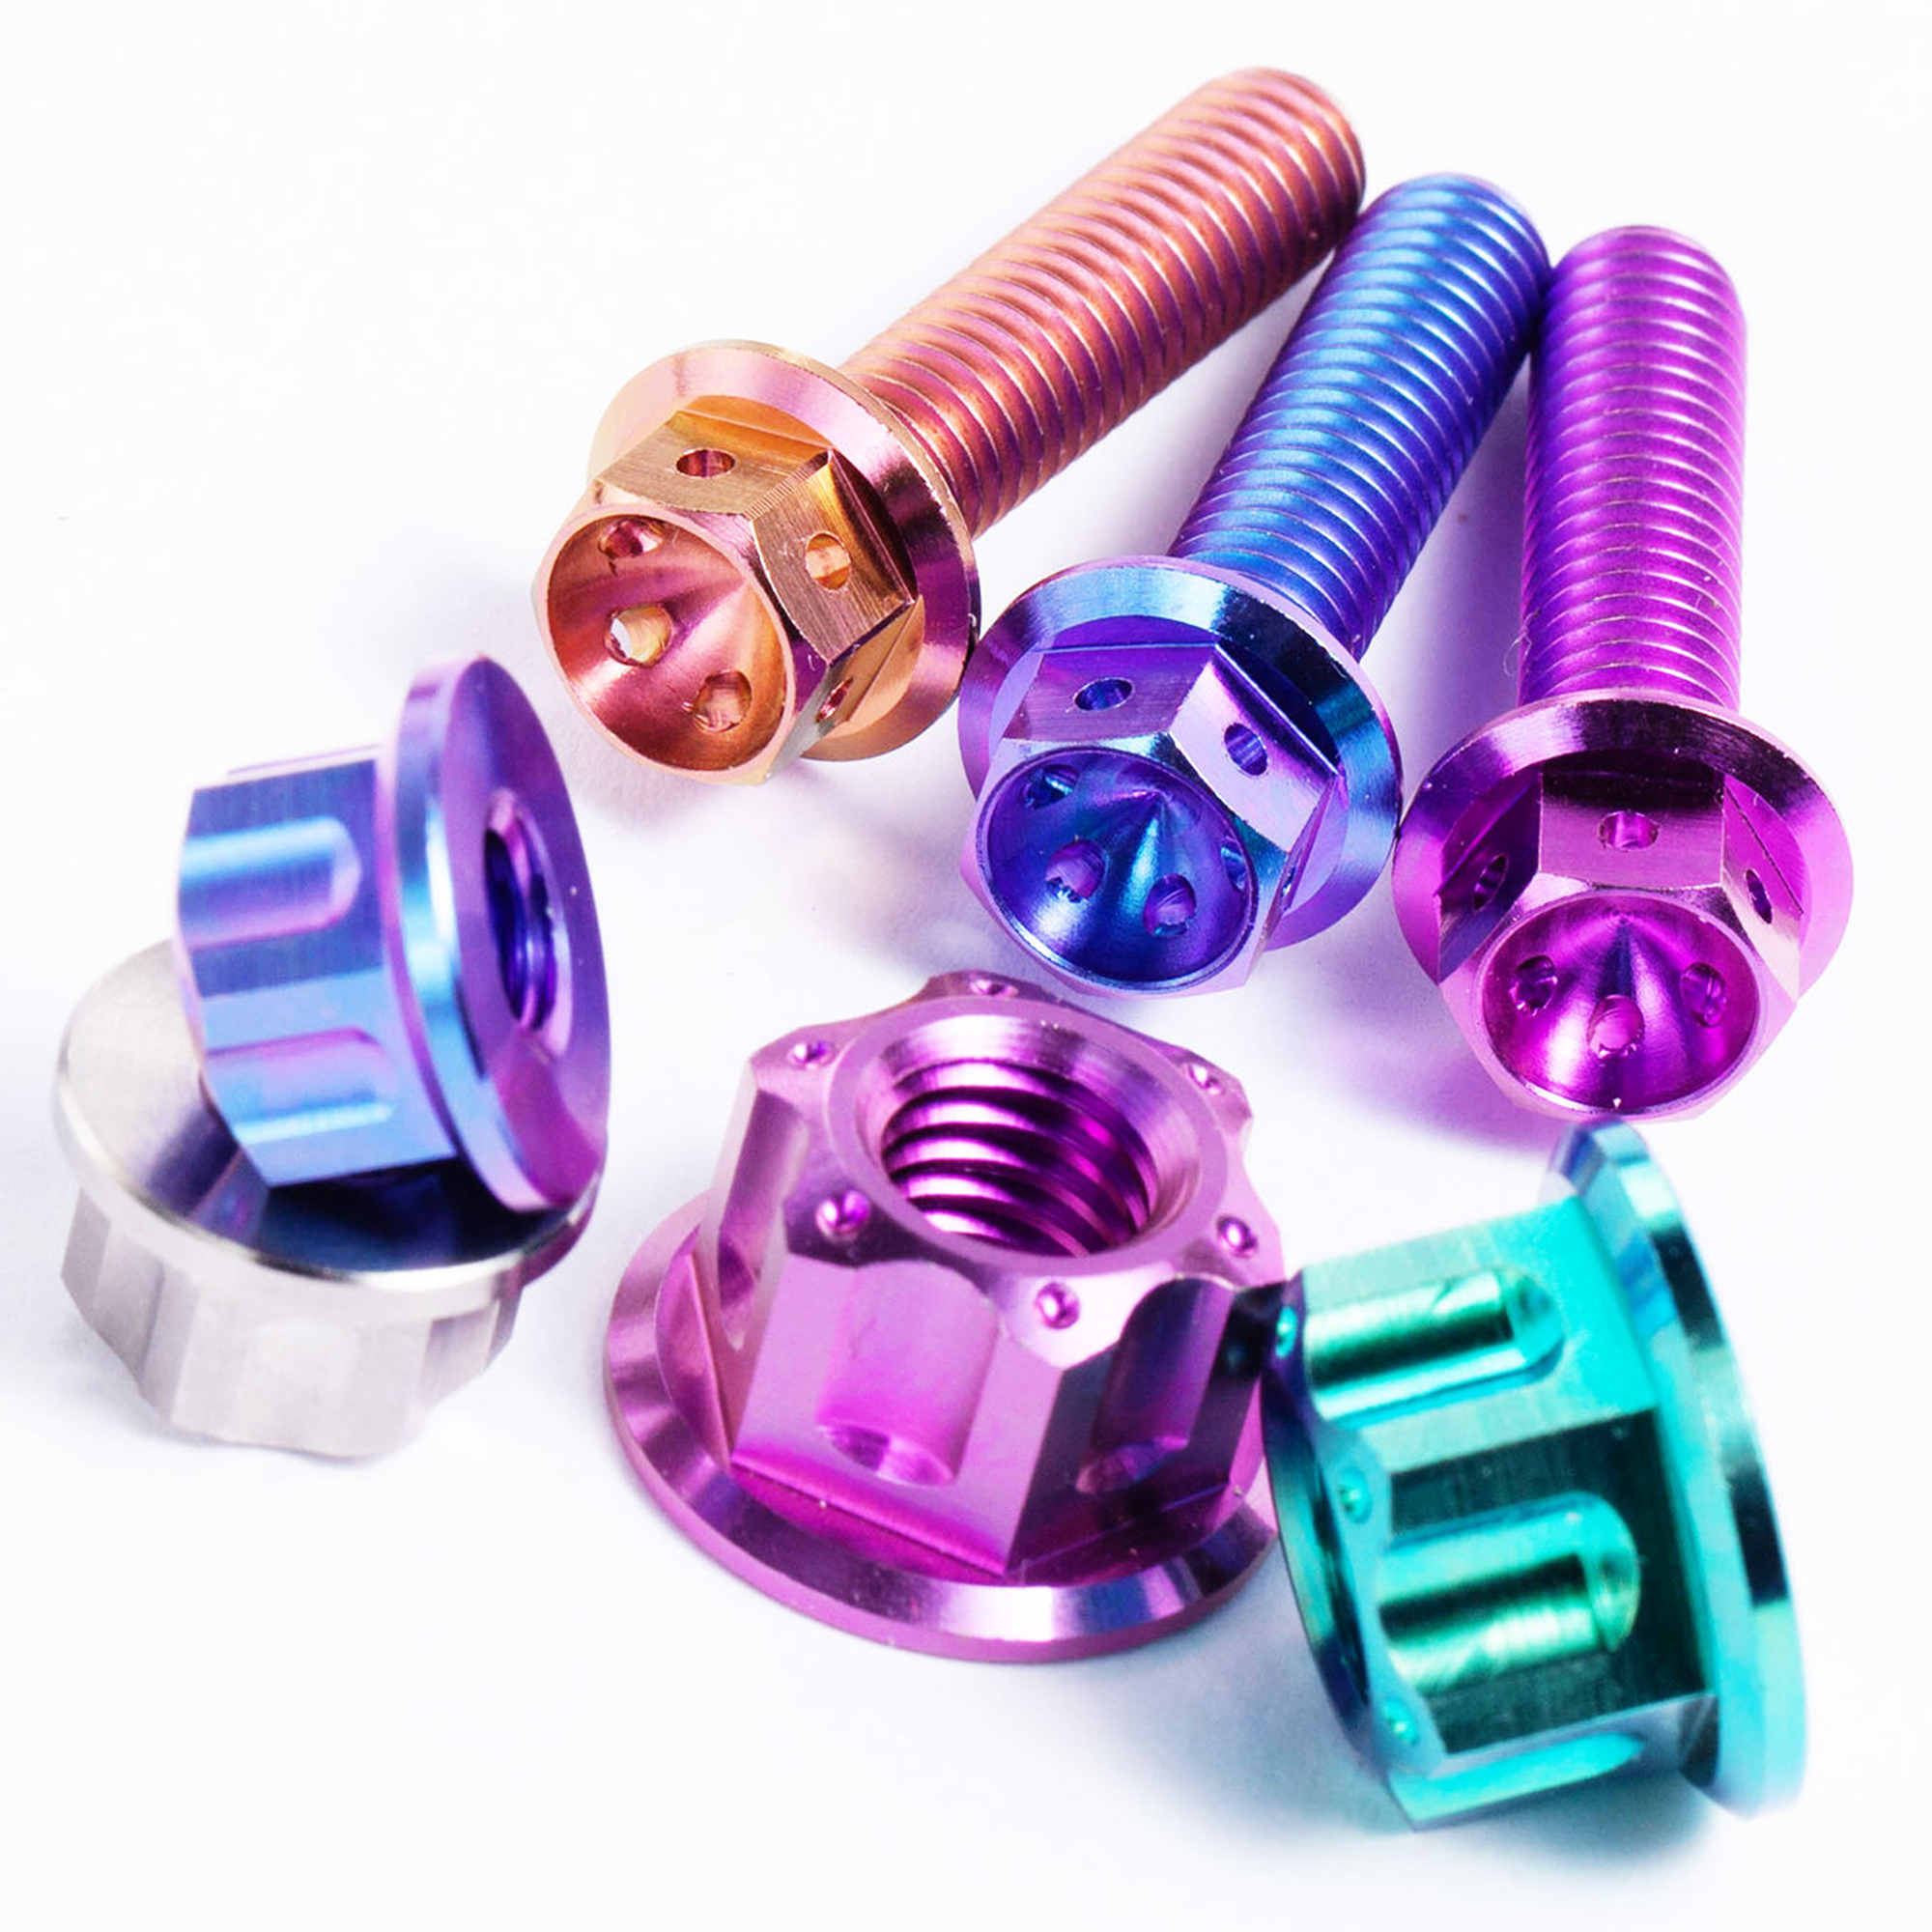
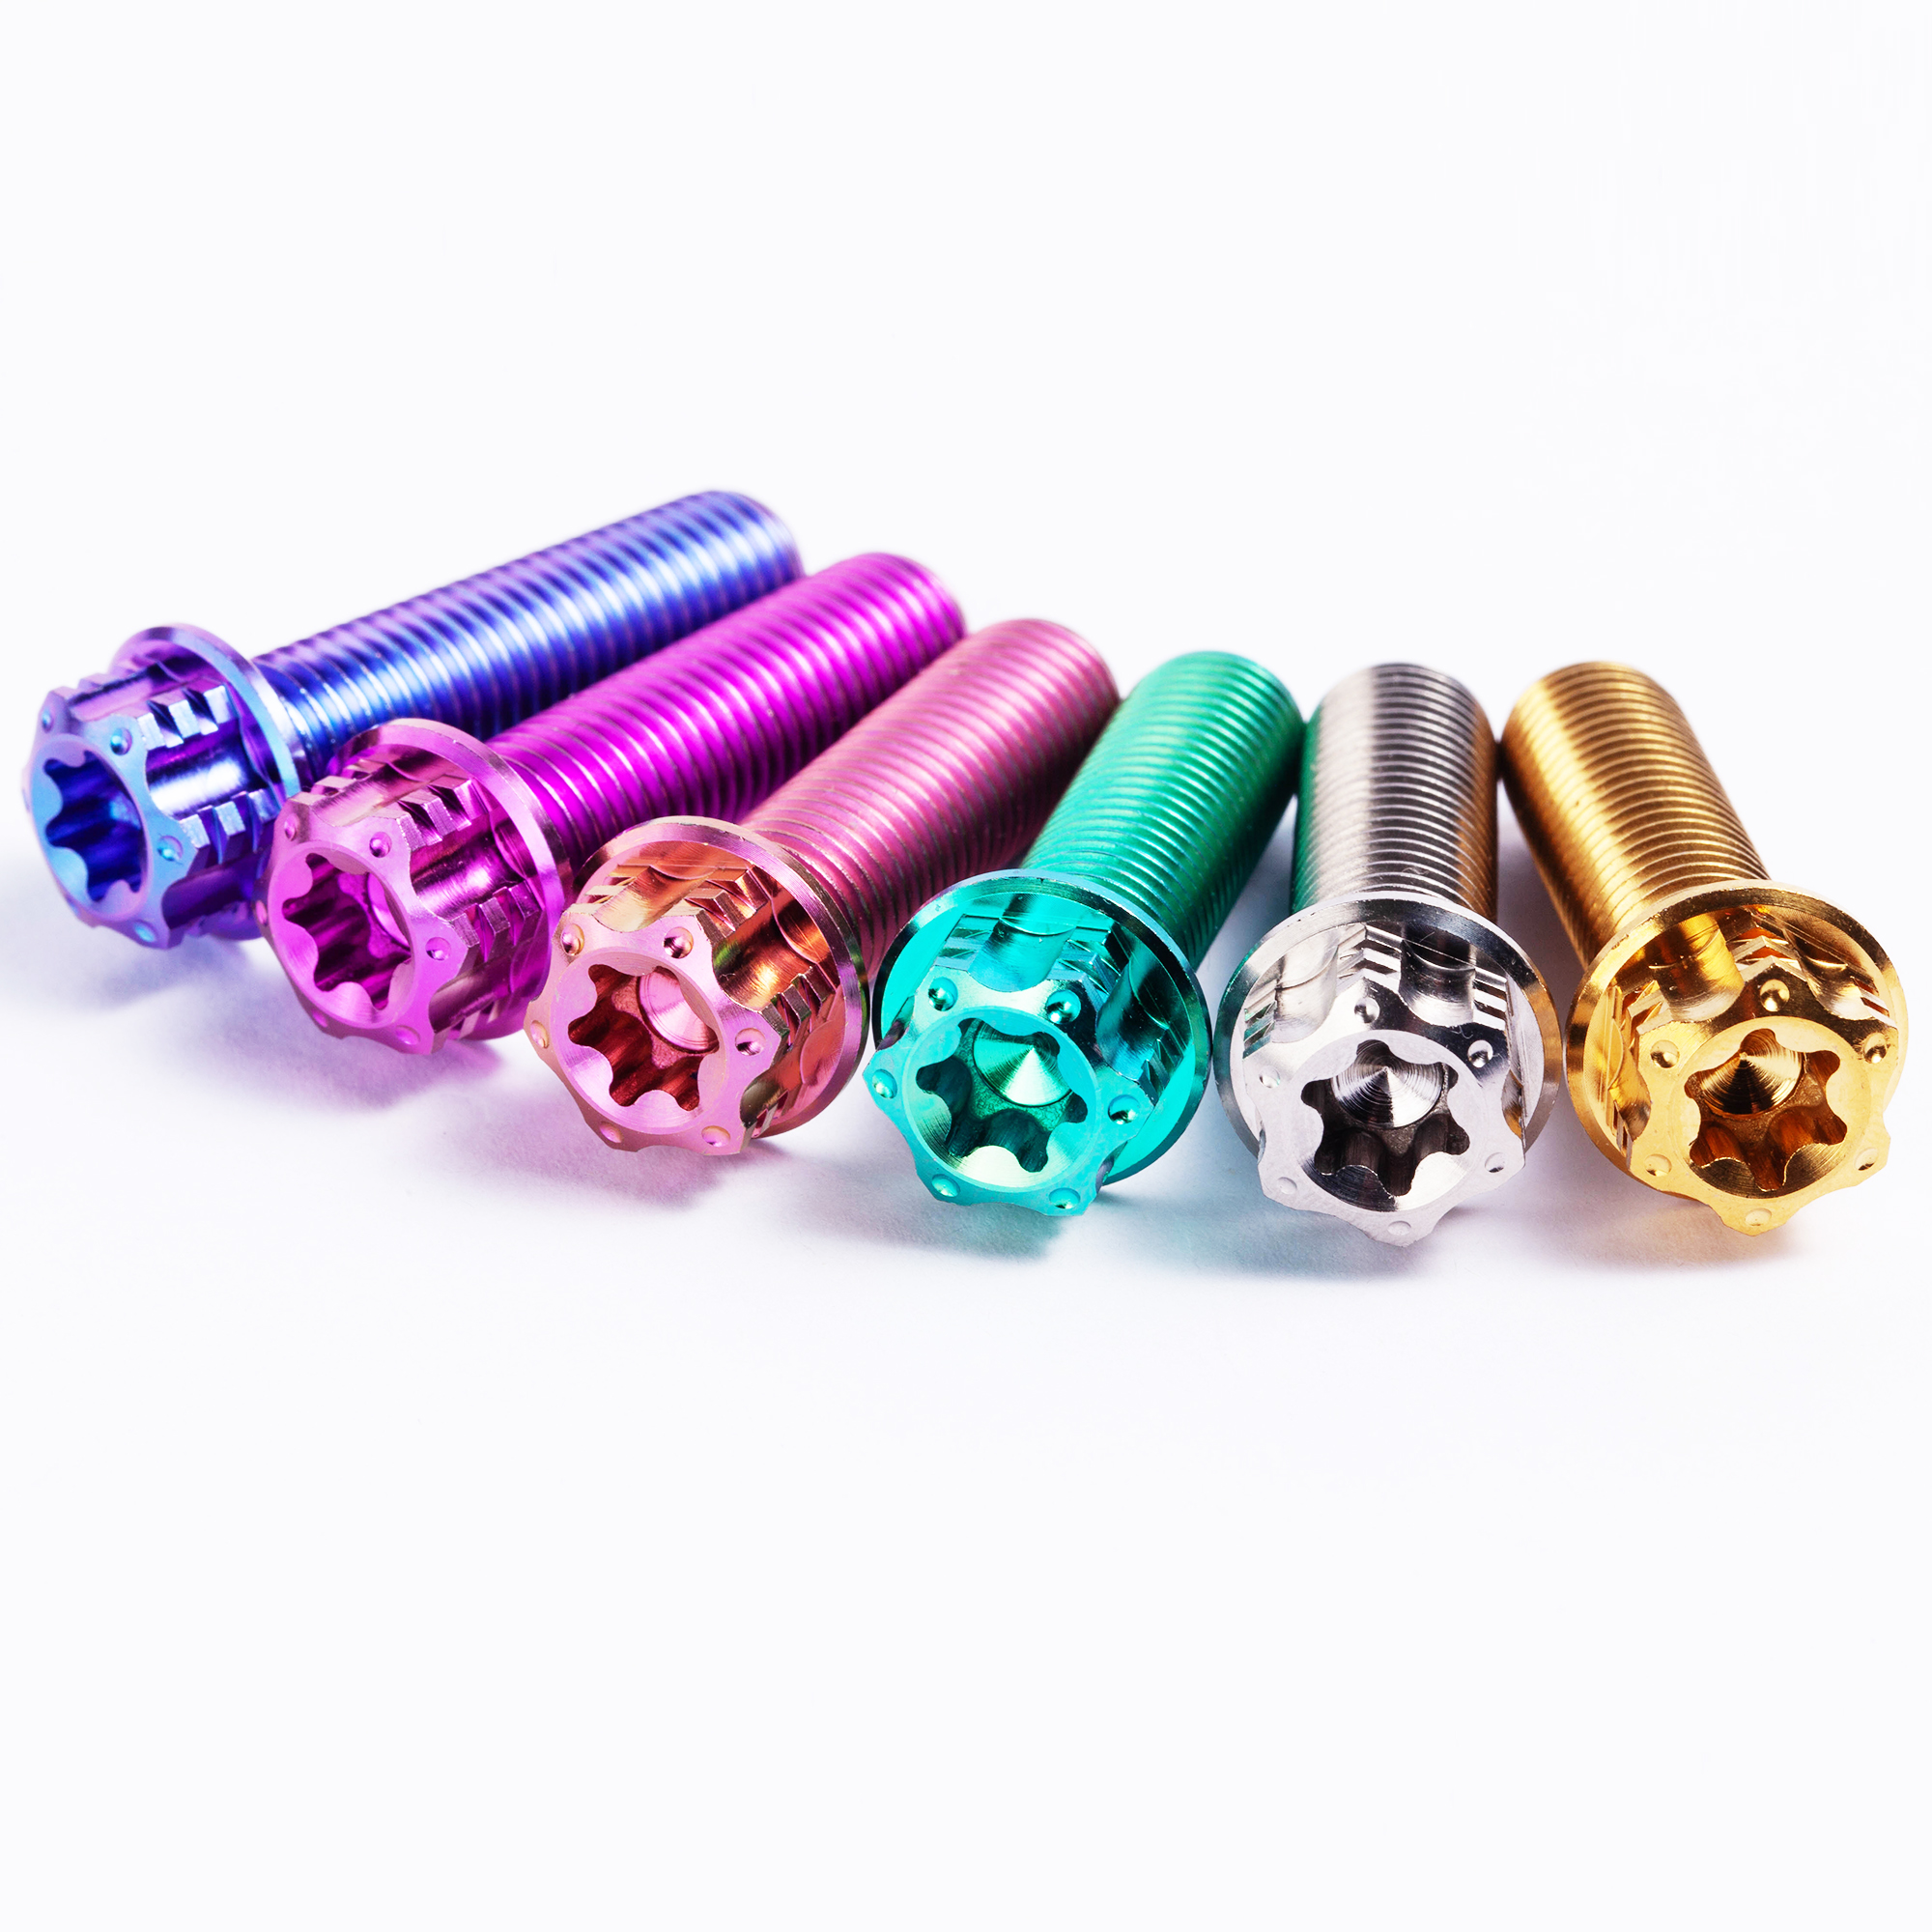
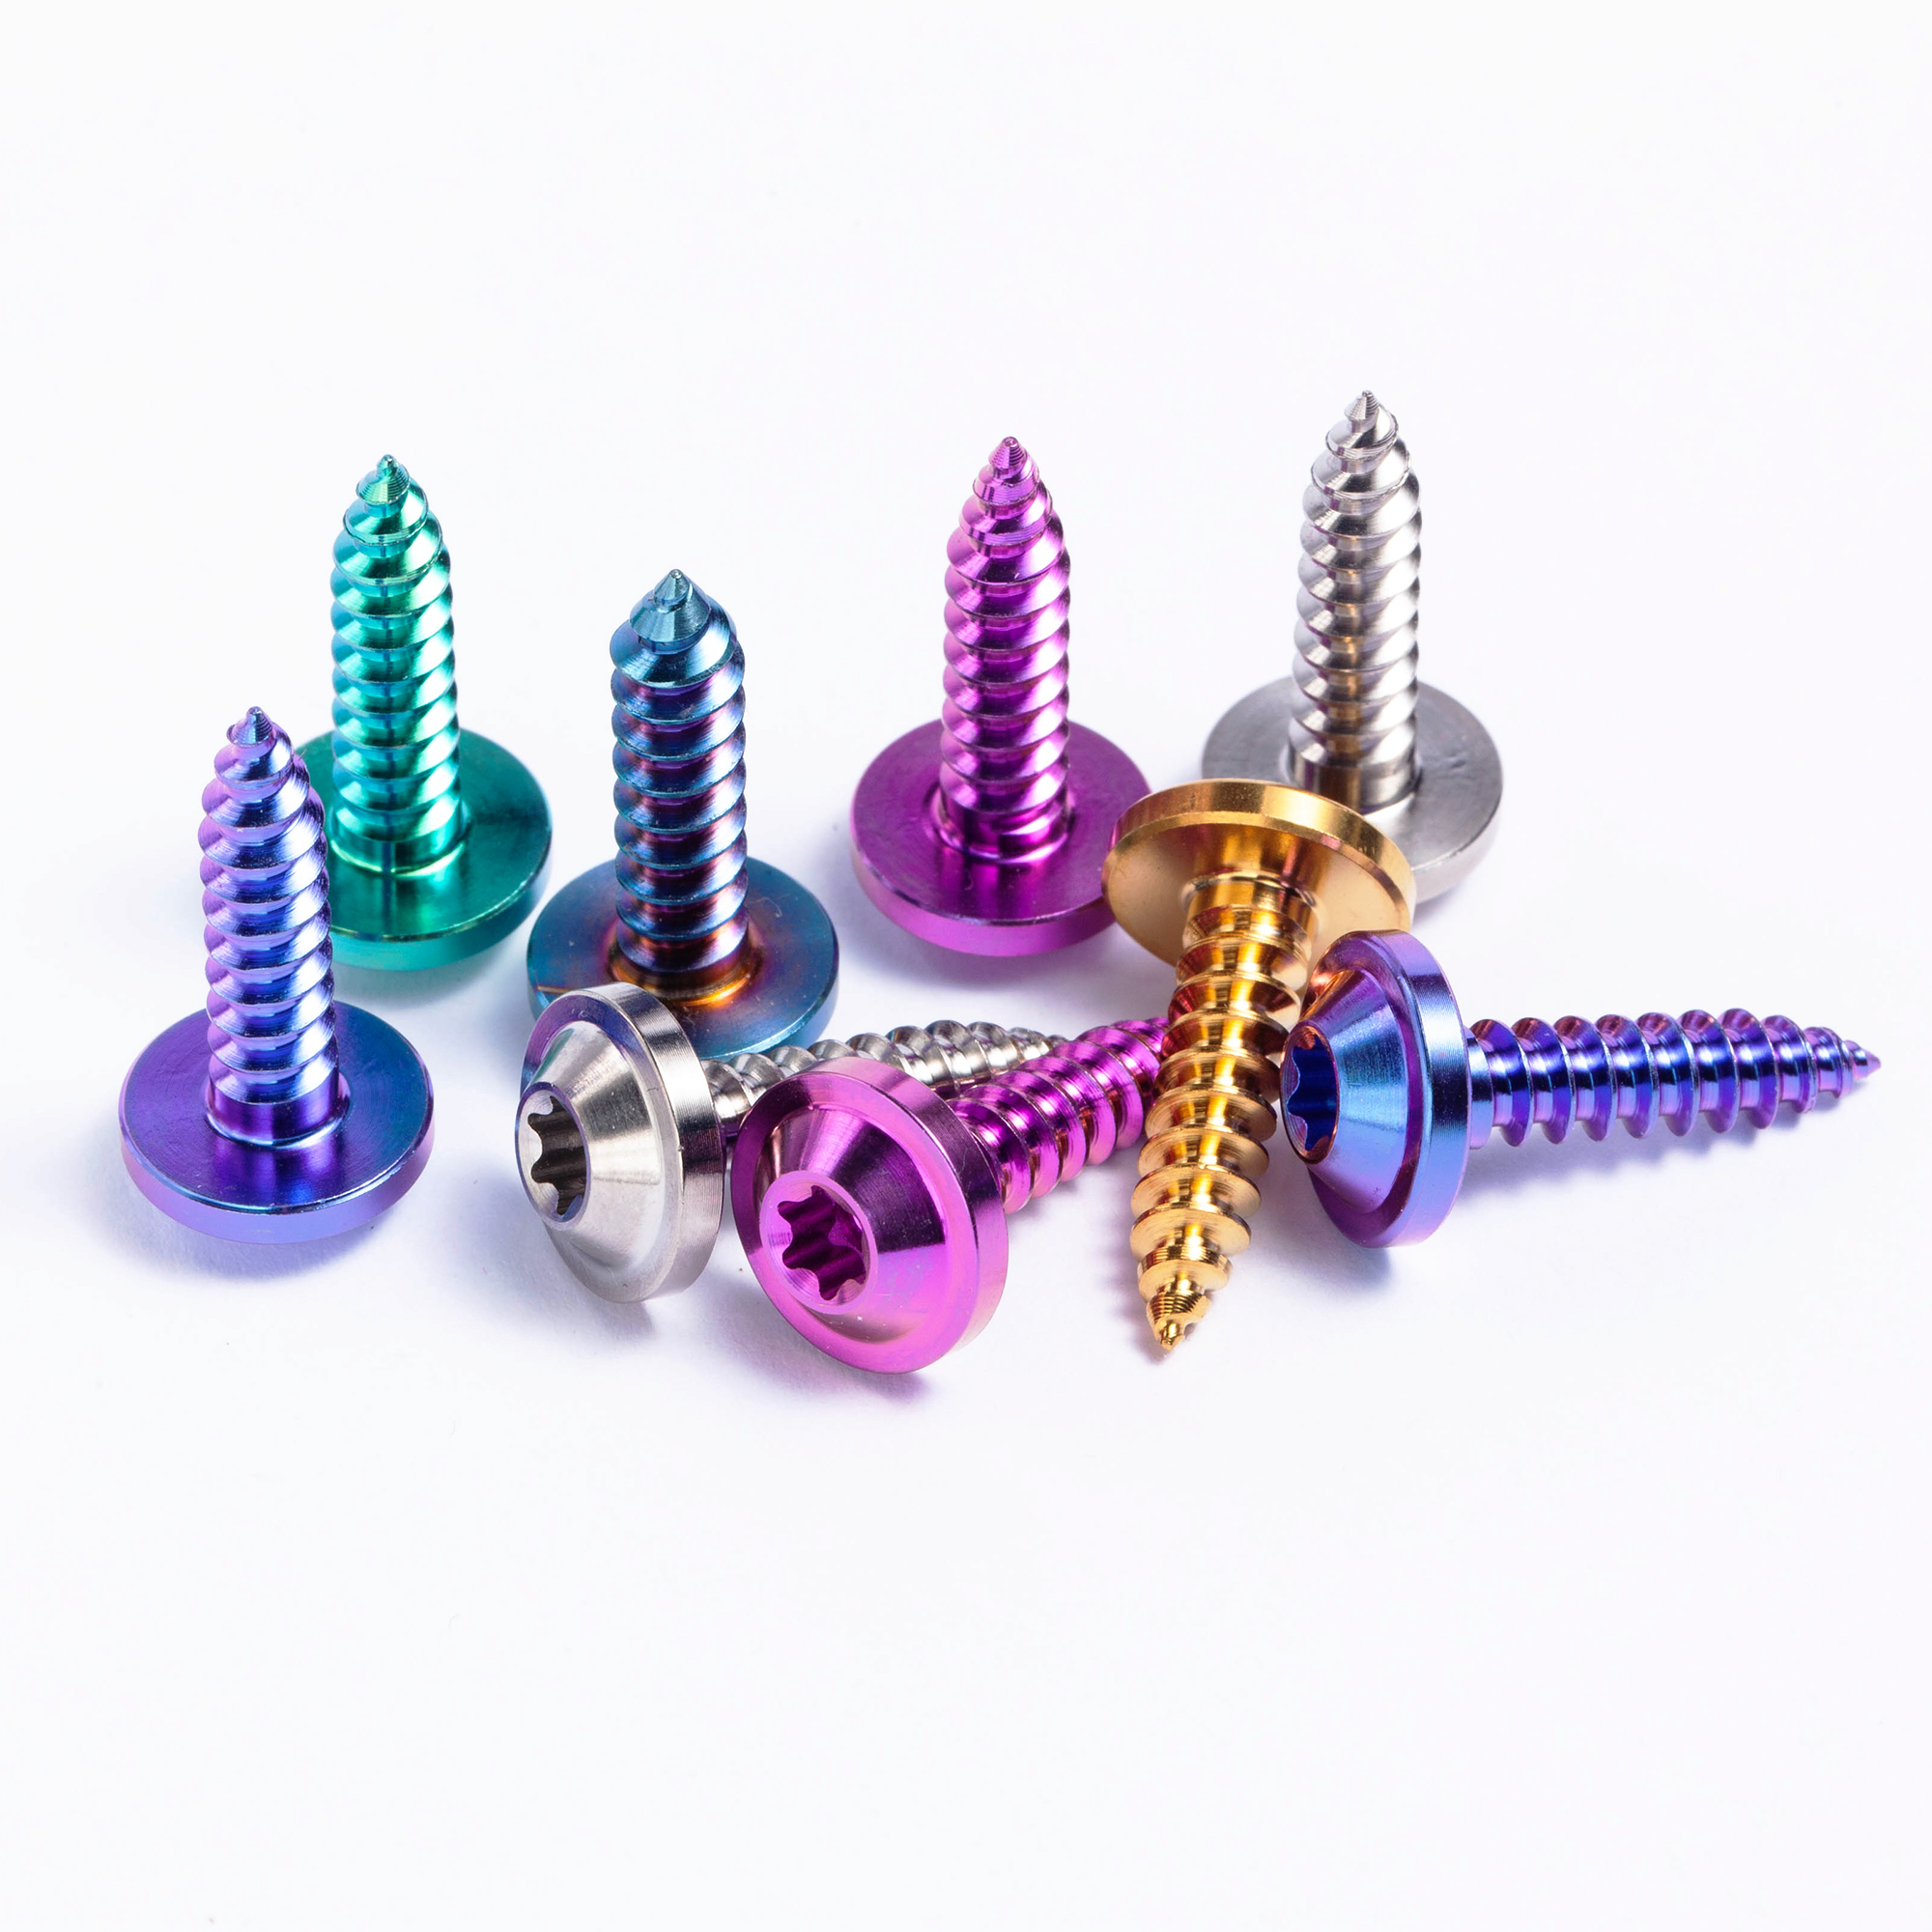
Metallurgical Fundamentals: Why Ti-6Al-4V Grade 5 and CP Grade 2 Dominate Exhaust Geometries
In high-performance exhaust manifold fabrication, turbocharger hot-side interconnections, and downpipe collector joints, standard 304 or 316L stainless steel flanges routinely reach structural and thermodynamic limits. Automotive engineers, dyno testing facilities, and specialized fabrication shops operating in Triesen, Vaduz, and the St. Gallen-Rheintal corridor demand extreme dimensional stability under cyclical thermal spikes exceeding 750°C (1,382°F).
Custom OEM titanium exhaust flanges engineered by Jiaxing Wexra Titanium Products Co., Ltd. are manufactured from certified titanium alloy bar stock and forged billets conformant to ASTM B348, ASTM B265, and AMS 4928 specifications. By leveraging Ti-6Al-4V (Grade 5) for high-clamping load applications and Commercially Pure Grade 2 (CP-Ti) for ductile, high-flow weldable ports, system designers achieve substantial benefits over ferrous metals:
- Density Optimization: Titanium possesses a density of approximately 4.43 g/cm³ compared to 7.93 g/cm³ for 304 austenitic stainless steel, yielding an instantaneous 44% mass reduction across exhaust hangars, collector flanges, and cylinder head transition plates.
- Thermal Expansion Compatibility: Titanium Grade 5 features a low coefficient of thermal expansion (α ≈ 8.6 × 10⁻⁶ K⁻¹ between 20°C and 500°C), roughly half that of 300-series stainless steel (16-18 × 10⁻⁶ K⁻¹). This drastically reduces cyclical gasket shear stress, prevents warping of manifold surfaces, and stops exhaust gas blow-by under wide-open-throttle (WOT) racing conditions.
- Fatigue Endurance Under Vibration: Alpine race courses, winding mountain inclines, and continuous vibration generate high cyclic harmonic loads on exhaust brackets and collector hardware. Titanium's fatigue limit ($S_e$) represents up to 55% of its ultimate tensile strength, compared to roughly 35-40% in structural automotive steels.
| Material Specification | Density (g/cm³) | Yield Strength $R_{p0.2}$ (MPa) | Tensile Strength $R_m$ (MPa) | CTE (20-500°C) ($10^{-6}/K$) | Primary Application Area |
|---|---|---|---|---|---|
| Titanium Grade 5 (Ti-6Al-4V) Aerospace / OEM | 4.43 | 828 | 895 - 1000 | 8.6 | Turbo manifold flanges, wastegate flanges, multi-bolt junctions |
| Titanium Grade 2 (CP-Ti) | 4.51 | 275 - 350 | 345 - 450 | 8.9 | Slip-fit exhaust collars, low-pressure merge collectors, tailpipe rings |
| Stainless Steel 304 / 1.4301 | 7.93 | 205 | 515 - 700 | 17.2 | Standard commercial exhaust flanges (prone to warping) |
| Stainless Steel 321 / 1.4541 (Stabilized) | 7.90 | 220 | 540 - 720 | 16.6 | Elevated-temperature steel systems (significantly higher mass) |
Localized Application Scenarios in Triesen and the Rhine Valley Industrial Cluster
Located on the eastern banks of the Alpine Rhine within the Principality of Liechtenstein, Triesen forms an essential node in the cross-border Central European precision engineering corridor connecting Buchs, Vaduz, Balzers, and Feldkirch. While Liechtenstein is globally renowned for specialized industrial tooling, thin-film coating technology, and acoustic-vibrational measuring instruments, local development centers and specialty tuning ateliers actively execute advanced thermal fluid dynamics research.
Bespoke Supercar Exhaust Fabrication
Private engineering shops throughout the Oberland region create custom inconel-titanium hybrid exhaust downpipes for bespoke sports cars. Our CNC milled Gr5 flanges ensure a flat, leak-proof seal without adding thermal mass to mid-engine compartments.
Hillclimb & Alpine Motorsport Dyno Testing
Regional racing entities competing in European Hillclimb Championships and VLN Endurance rely on precision CNC machined flanges that withstand violent thermal cycling on mountain pass stages without cracking the manifold headers.
Acoustic Tuning & Flow Benches
Liechtenstein's acoustic measurement engineers utilize titanium's distinctive sound attenuation curve. Custom precision port geometries prevent turbulence spikes at the cylinder exhaust interface during dynamometer validation.
Market & Regulatory Trends Impacting Triesen Automotive Buyers
Procurement teams and mechanical system architects across Liechtenstein, Switzerland, and Austria navigate increasingly stringent ecological and technical benchmarks. The integration of high-performance custom titanium components in performance exhaust tracts is driven by three distinct macro forces:
1. Euro 7 Readiness & Catalytic Light-Off Efficiency: Modern emissions standards require catalytic converters to achieve operating temperature in record time following a cold start. Ferrous exhaust flanges act as thermal heat sinks, siphoning critical heat away from the exhaust stream before it reaches the catalytic matrix. Titanium's significantly lower volumetric heat capacity ($C_v$) ensures rapid thermal transfer into emissions scrubbers, aiding compliance certification.
2. Hybridization Weight Budget Offsets: As hybrid powertrains integrate heavy 400V/800V battery packs and electric motor-generators (MGU-K) into modern chassis architectures, every gram in the ancillary combustion loop must be stripped out. Upgrading from multi-piece stainless steel exhaust flanges to monolithic, lightened Grade 5 titanium flanges recovers critical kilograms from the vehicle's overhang areas, optimizing polar moment of inertia.
3. Advanced CAD/CAM Prototyping and Fast-Turnaround Sourcing: The DACH automotive ecosystem thrives on agility. Long gone are 16-week lead times for tooling-intensive stamped parts. Triesen development teams now supply STEP, Parasolid, or IGES models directly to our facility for 5-axis CNC machining, contour waterjet cutting, and wire-EDM fabrication, receiving completed parts with dimensional reports within short production cycles.
Jiaxing Wexra Titanium: Advanced CNC Capabilities & Quality Architecture
Operating a modernized, titanium-dedicated facility with over 1,000 square meters of production space, Jiaxing Wexra Titanium Products Co., Ltd. (founded 2018) provides end-to-end control from raw ingot to final certified assembly.
High-Precision Multi-Axis Milling
Our fleet of rigid CNC centers maintains tolerances down to ±0.01 mm. Flange sealing faces undergo single-pass fly-cutting to achieve surface roughness finishes of Ra ≤ 0.8 μm, guaranteeing airtight metal-to-metal or embossed-gasket sealing.
Laser Profiling & Stress Relief
Advanced fiber laser cutting units slice titanium plates up to 20mm thickness with minimum heat-affected zones (HAZ). All pre-cut blanks undergo controlled vacuum annealing to eliminate residual rolling stresses before precision machining.
Spectrometric & Dimensional Audit
Every raw material batch is checked via direct-reading emission spectrometers (OES) and oxygen/nitrogen analyzers. CMM coordinate measuring machines and digital optical projectors verify hole pitches and bolt circle diameters (PCD).
Frequently Asked Questions: Sourcing Titanium Exhaust Flanges in Triesen, Liechtenstein
Clear, unvarnished guidance addressing customs frameworks, logistics, metallurgy, and fabrication standards for sourcing directors in the Rhine Valley.
Liechtenstein shares a common customs territory and monetary treaty with Switzerland (Swiss Customs Union). Shipments sent from our facility via air express (DHL/FedEx/TNT) or freight forwarders clear customs through Swiss customs checkpoints (e.g., Zurich Airport or Basel). Wexra provides all required commercial export documentation, HS Tariff Codes (typically under HS 8108.90 for wrought titanium articles), and declaration of origin, allowing seamless DDP or DAP delivery directly to your facility in Triesen without unnecessary regional delays.
For structural bolt-down flanges—such as turbo inlet/outlet flanges, engine head exhaust manifold plates, and two-bolt/three-bolt collector interfaces—Grade 5 (Ti-6Al-4V) is standard. Its high yield strength (828 MPa) resists flange bending under high bolt clamping torques. Conversely, Grade 2 is preferred for lightweight exhaust tips, secondary slip-fit sleeves, or applications where intricate press-forming and straightforward TIG welding without specialized pre-heating are prioritized.
In accordance with European quality auditing norms, every production lot can be supplied with an Inspection Certificate conforming to DIN EN 10204 Type 3.1. This document specifies precise chemical heat composition (Al, V, Fe, C, N, H, O levels) and mechanical tensile test data. Furthermore, Wexra maintains certified adherence to ISO 9001:2015, RoHS, and EU REACH chemical safety guidelines, alongside full dimensional inspection protocol sheets.
Titanium has a relatively low thermal conductivity ($k \approx 6.7 \text{ W/m}\cdot\text{K}$ for Gr5 compared to $\approx 16 \text{ W/m}\cdot\text{K}$ for stainless steel). Concentrated machining heat can induce localized stress. We employ optimized high-pressure through-spindle coolant, climb-milling strategies, and sharp, dedicated carbide tooling. For high-thickness flanges, intermediate stress-relief heat treatment is conducted prior to final finish skim passes, securing flatness across bolt lines within 0.05 mm.
We provide natural micro-machined, vibratory tumbled, fine bead-blasted, and high-mirror polished surfaces. For aesthetic and heat-protective applications, we offer Type II electrochemical anodizing in distinct hues (gold, purple, cyan, burnt-blue) and vacuum PVD (Physical Vapor Deposition) coatings. Our anodization process modifies the natural surface oxide crystal matrix ($TiO_2$) without adding measurable coating thickness, ensuring critical thread and bolt clearance tolerances remain intact.
From Digital CAD Model to Liechtenstein Facility: 5-Stage Controlled Sourcing
To eliminate scrap rates and bridge geographic distances, our engineering workflow integrates checkpoints aligned with European automotive VDA / PPAP principles:
1. DFM & CAD Review
Clients upload STEP/DXF files. Our engineering staff assesses tool access, thermal port radii, chamfer clearances, and material yield to ensure cost efficiency.
2. Billet Traceability
Certified vacuum-arc remelted (VAR) Gr2 or Gr5 raw titanium is cut and linked to its mill heat batch number. Spectrometric verification precedes machining.
3. 5-Axis CNC Milling
Flange bolt patterns, O-ring gasket counterbores, and port transitions are machined in single setups to safeguard concentricity and perpendicularity.
4. Metrology & Leak Testing
Flange surfaces are checked for planar flatness. Thread profiles undergo gauge go/no-go checks. Dimensional inspection reports are created.
5. Clean Packaging & Alpine Express Air Logistics
Finished flanges are ultrasonically cleaned, individually vacuum-sealed in protective corrosion-inhibiting poly bags to avoid freight abrasions, and dispatched via express air directly to your delivery address in Triesen, FL.
Ready to Engineer High-Thermal Titanium Flanges for Your Next Project?
Whether you require a low-volume prototyping run for prototype dyno evaluation in Triesen or scheduled serial production for aftermarket distribution across Europe, our engineering desk delivers quotes and DFM feedback within 8 working hours.
Get Catalog