44%
Weight Reduction vs. Steel
±0.01mm
CNC Machining Tolerance
895+ MPa
Ti-6Al-4V Tensile Strength
100%
CE, RoHS & REACH Traceable
High-Performance Titanium Hardware Portfolio
Engineered for extreme cyclical loading, elevated thermal thresholds, and weight-sensitive dynamic components.
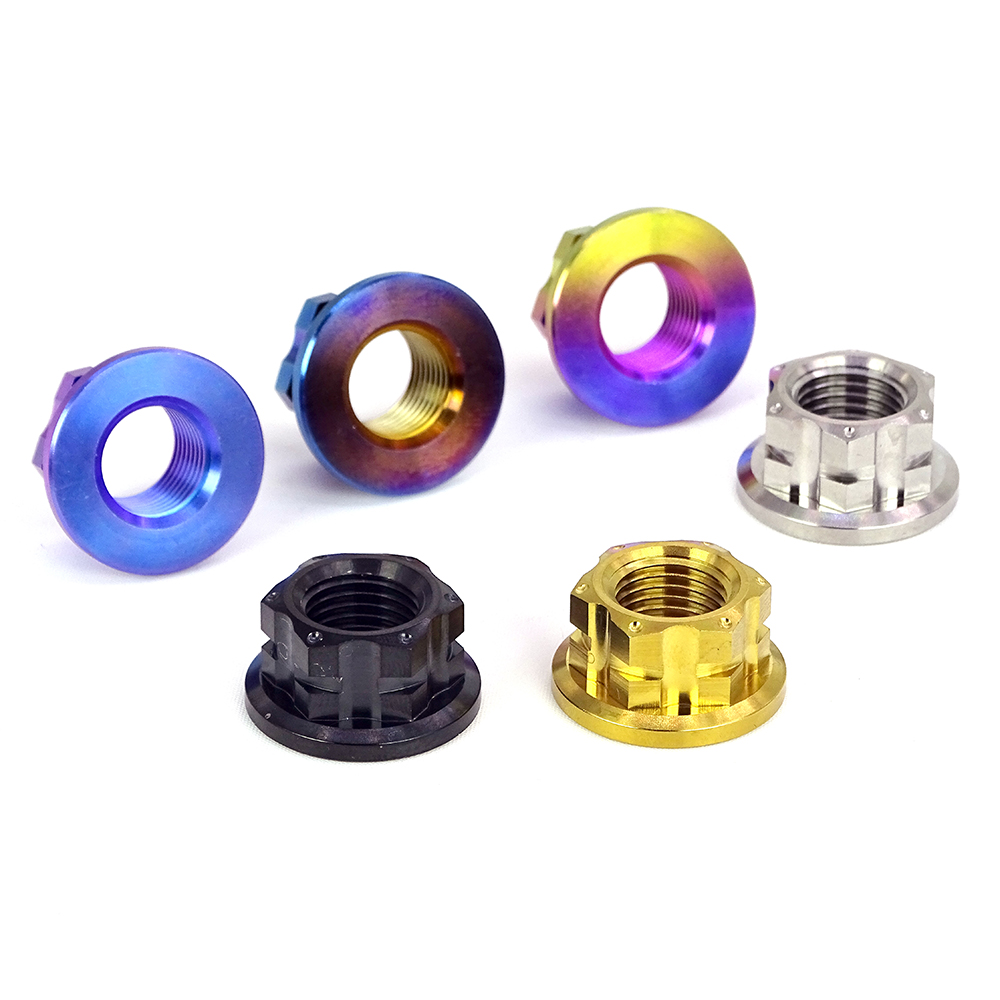
Motorcycle Electric Car Modified Titanium Alloy Fancy Hex Flange Nut
Explore Product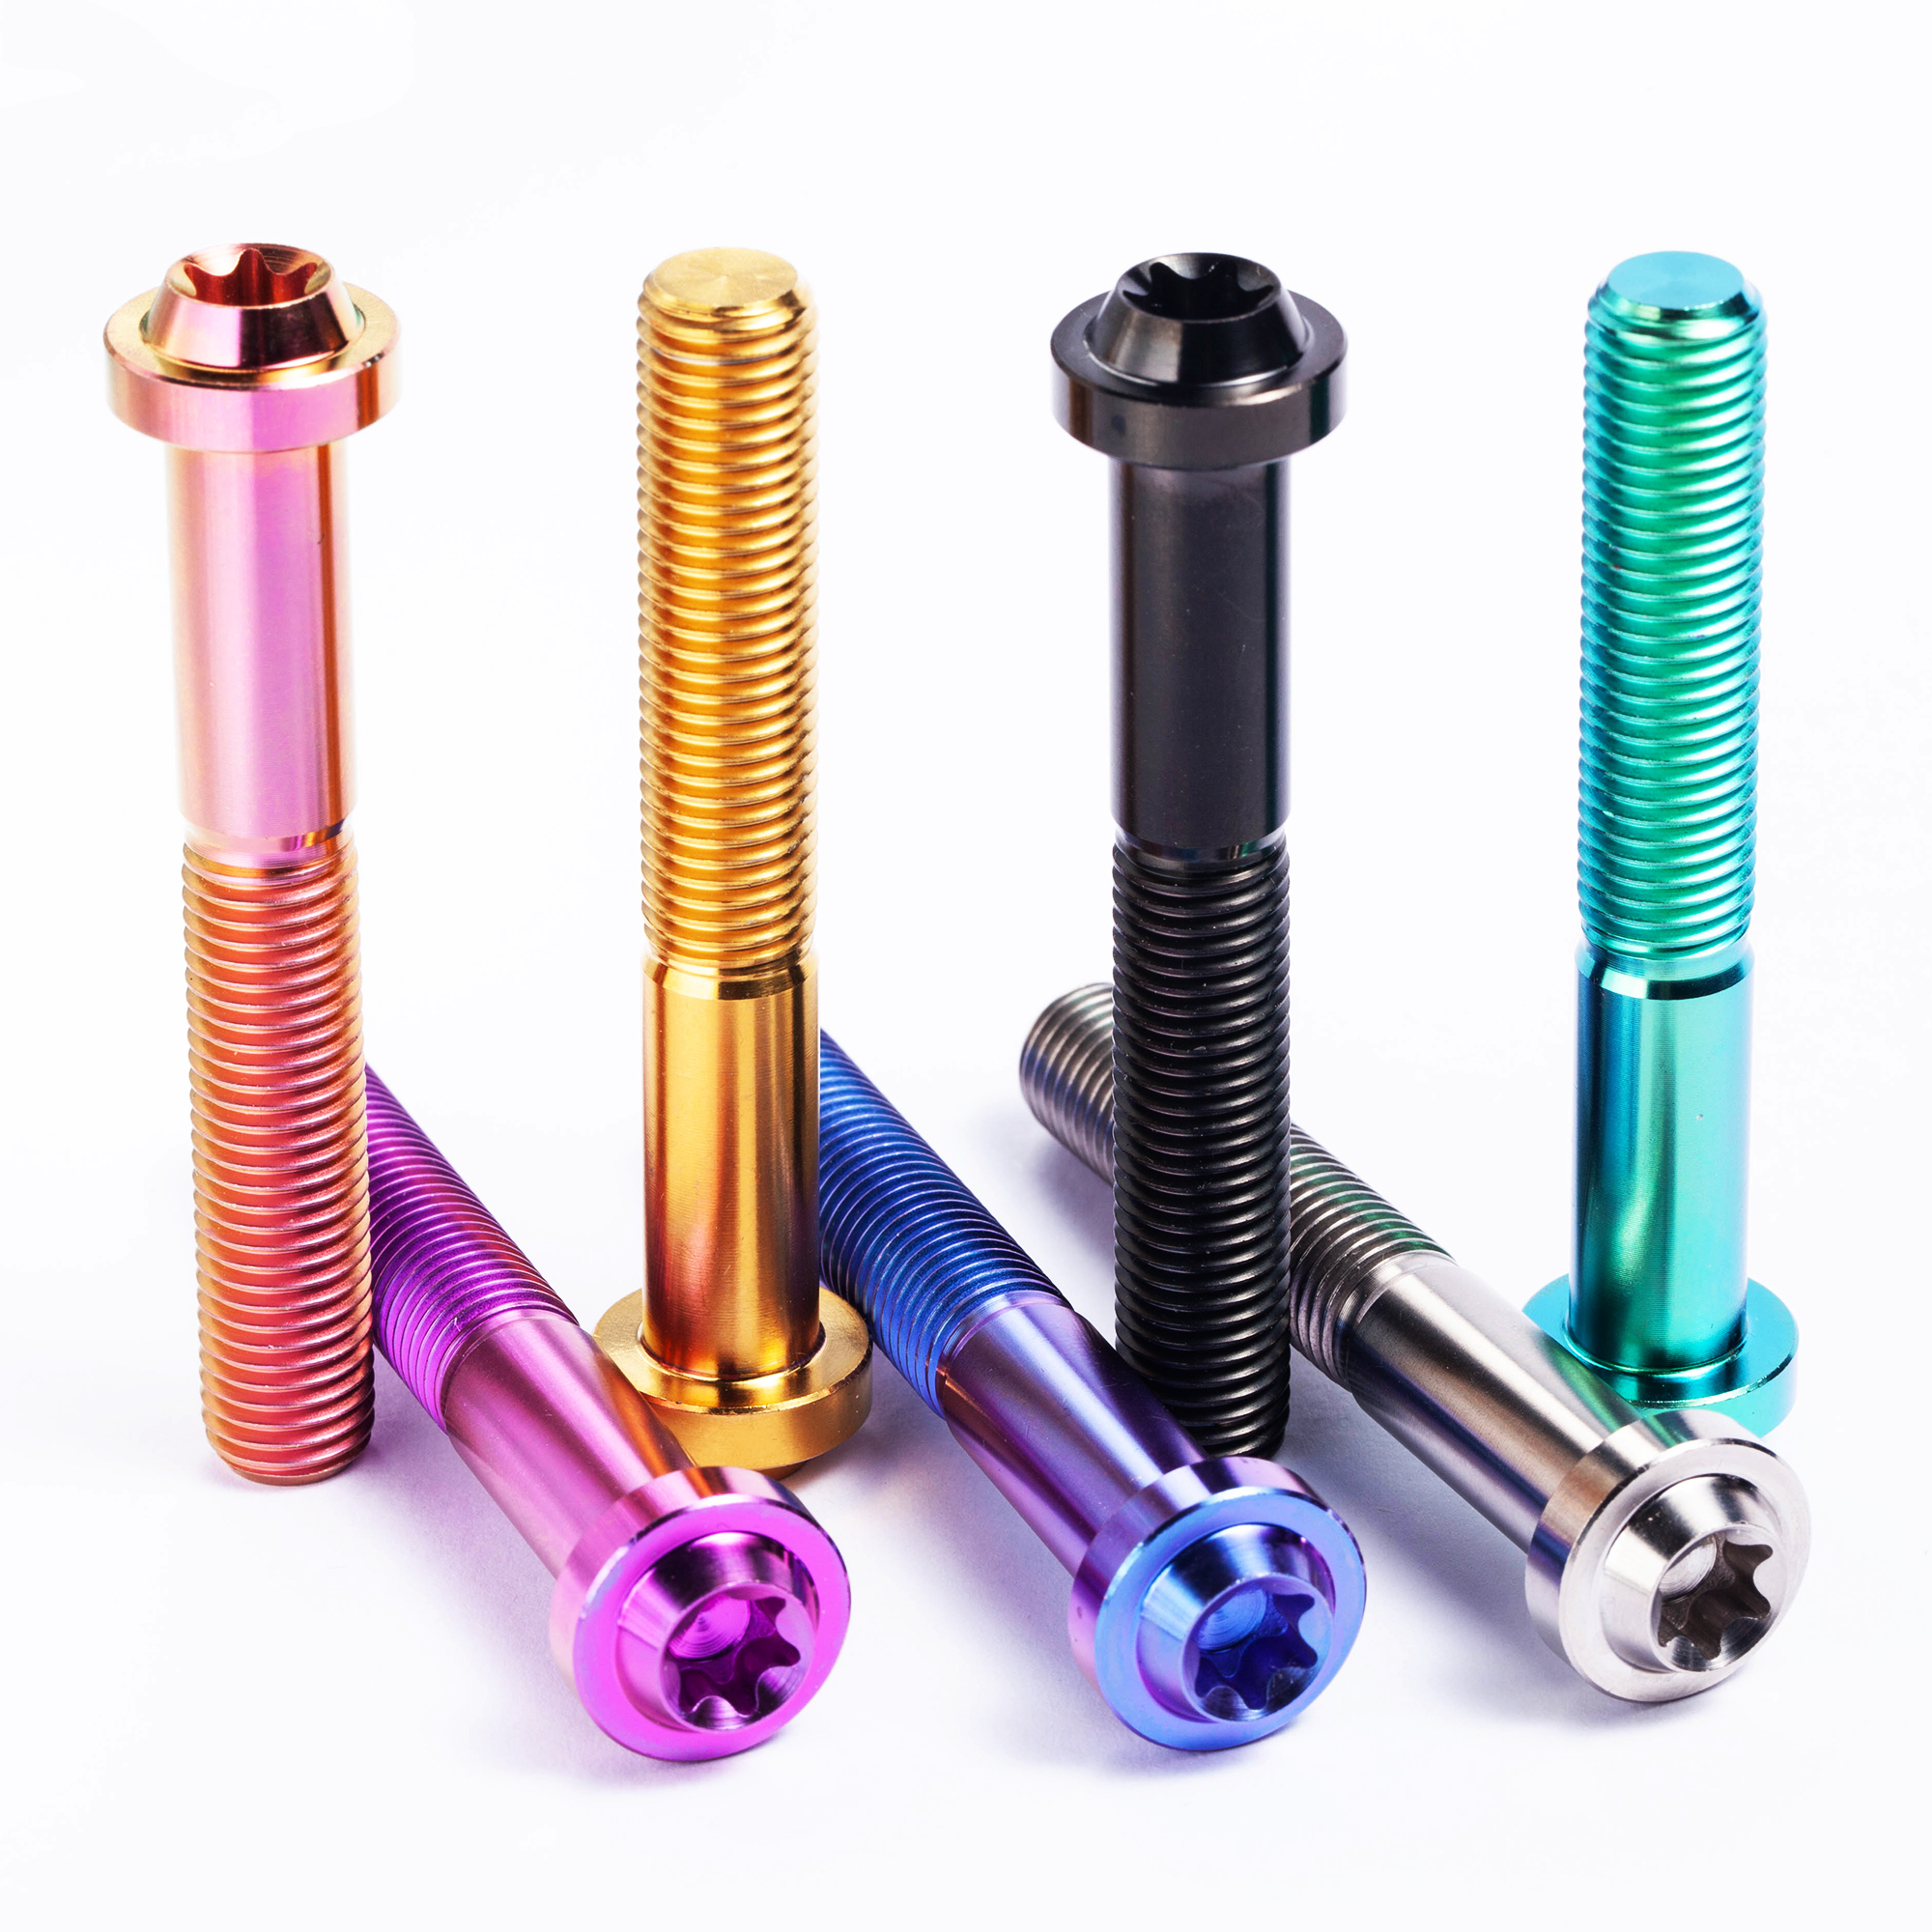
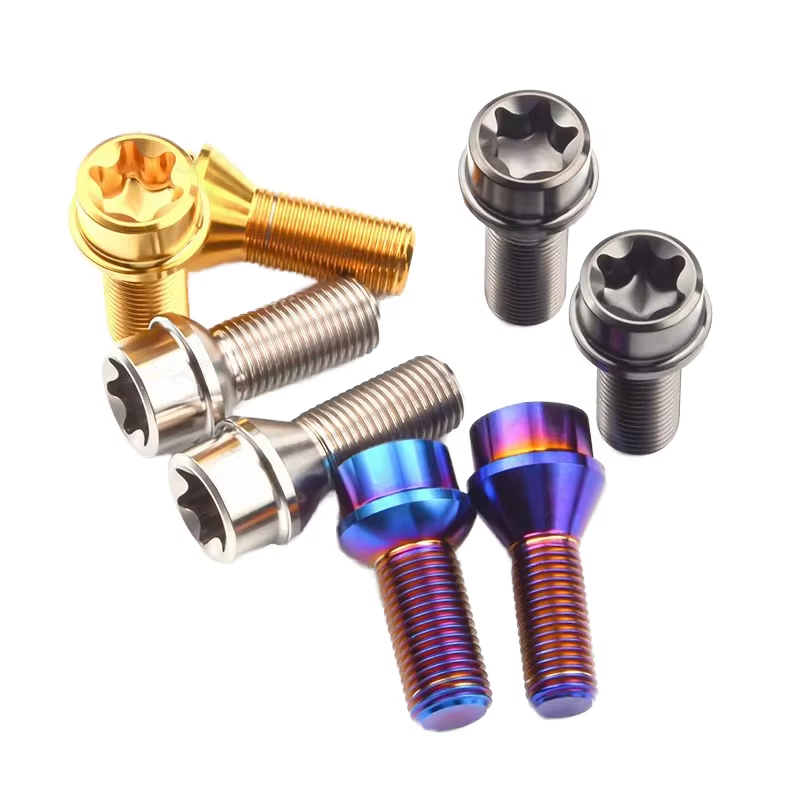
DIN912 Metric Bolts M2-M8 Grade 9 / Grade 5 Titanium Standard Fasteners
Explore Product
LENS 13 Optical Grade PVC Lamp Multi-Color Optimum Performance Unit
Explore Product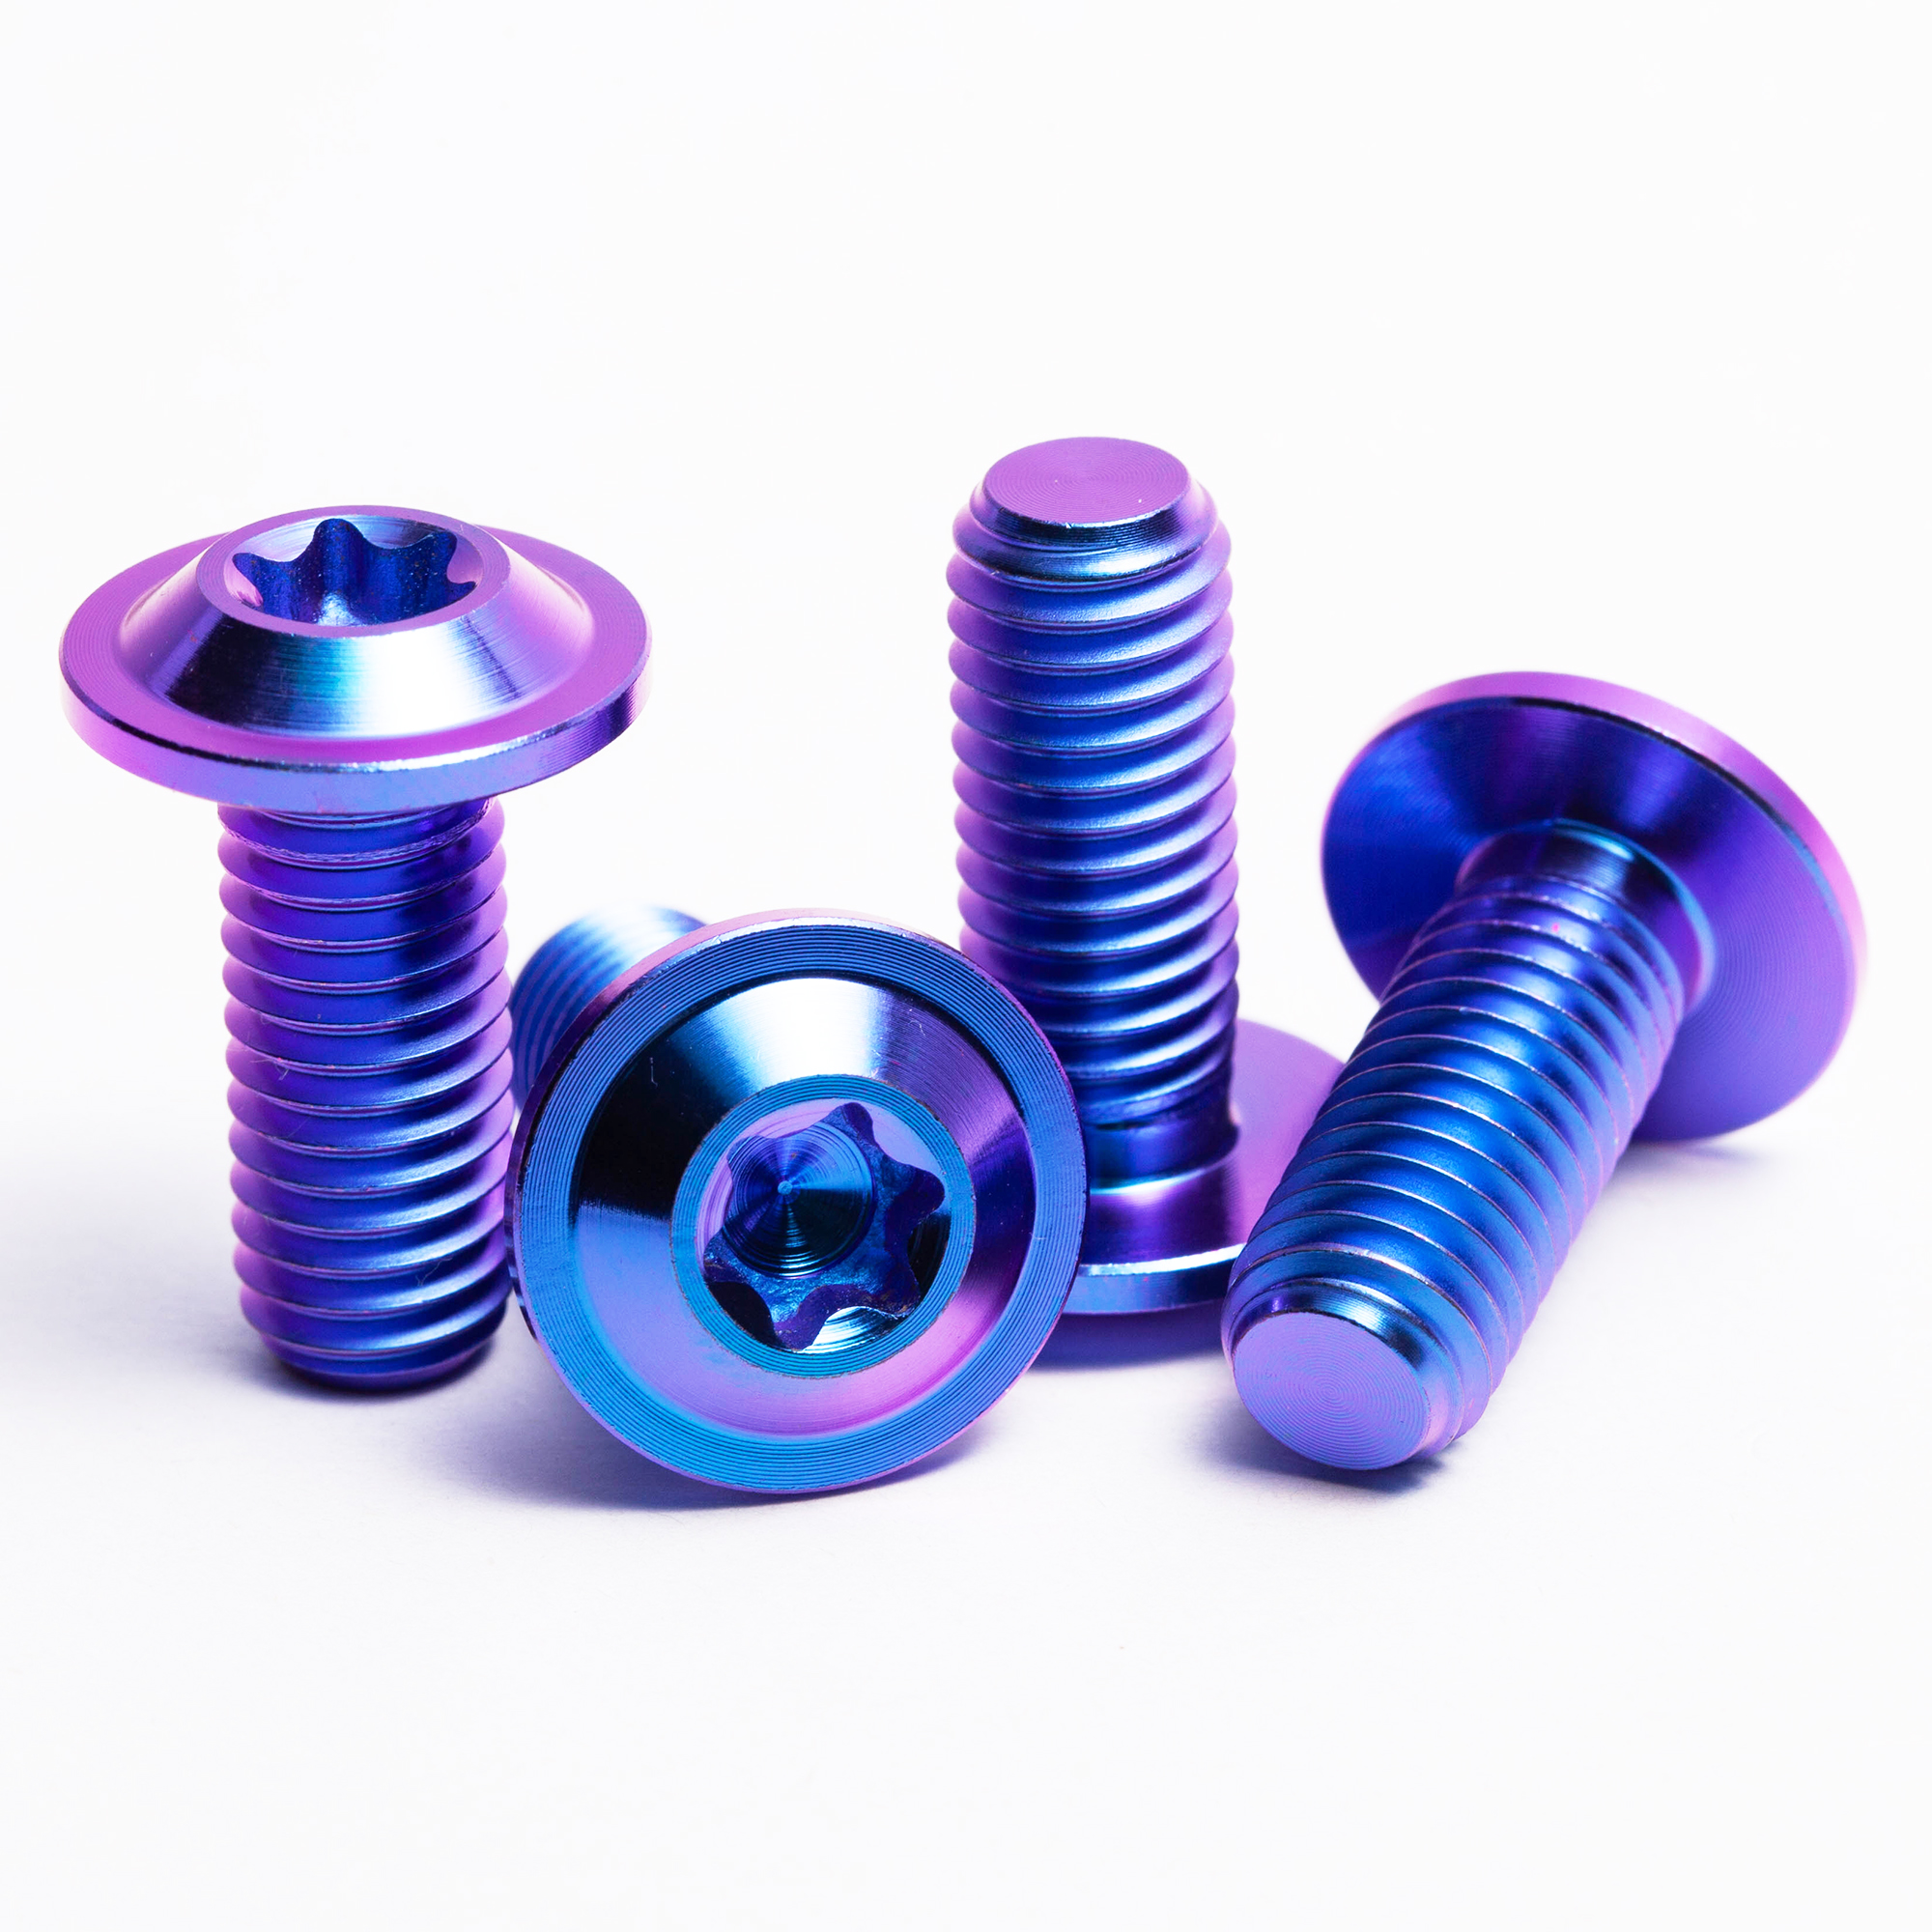
Customized Titanium Disc Head Bolts M6/M8/M10 Gr5 DIN6921 Screws
Explore Product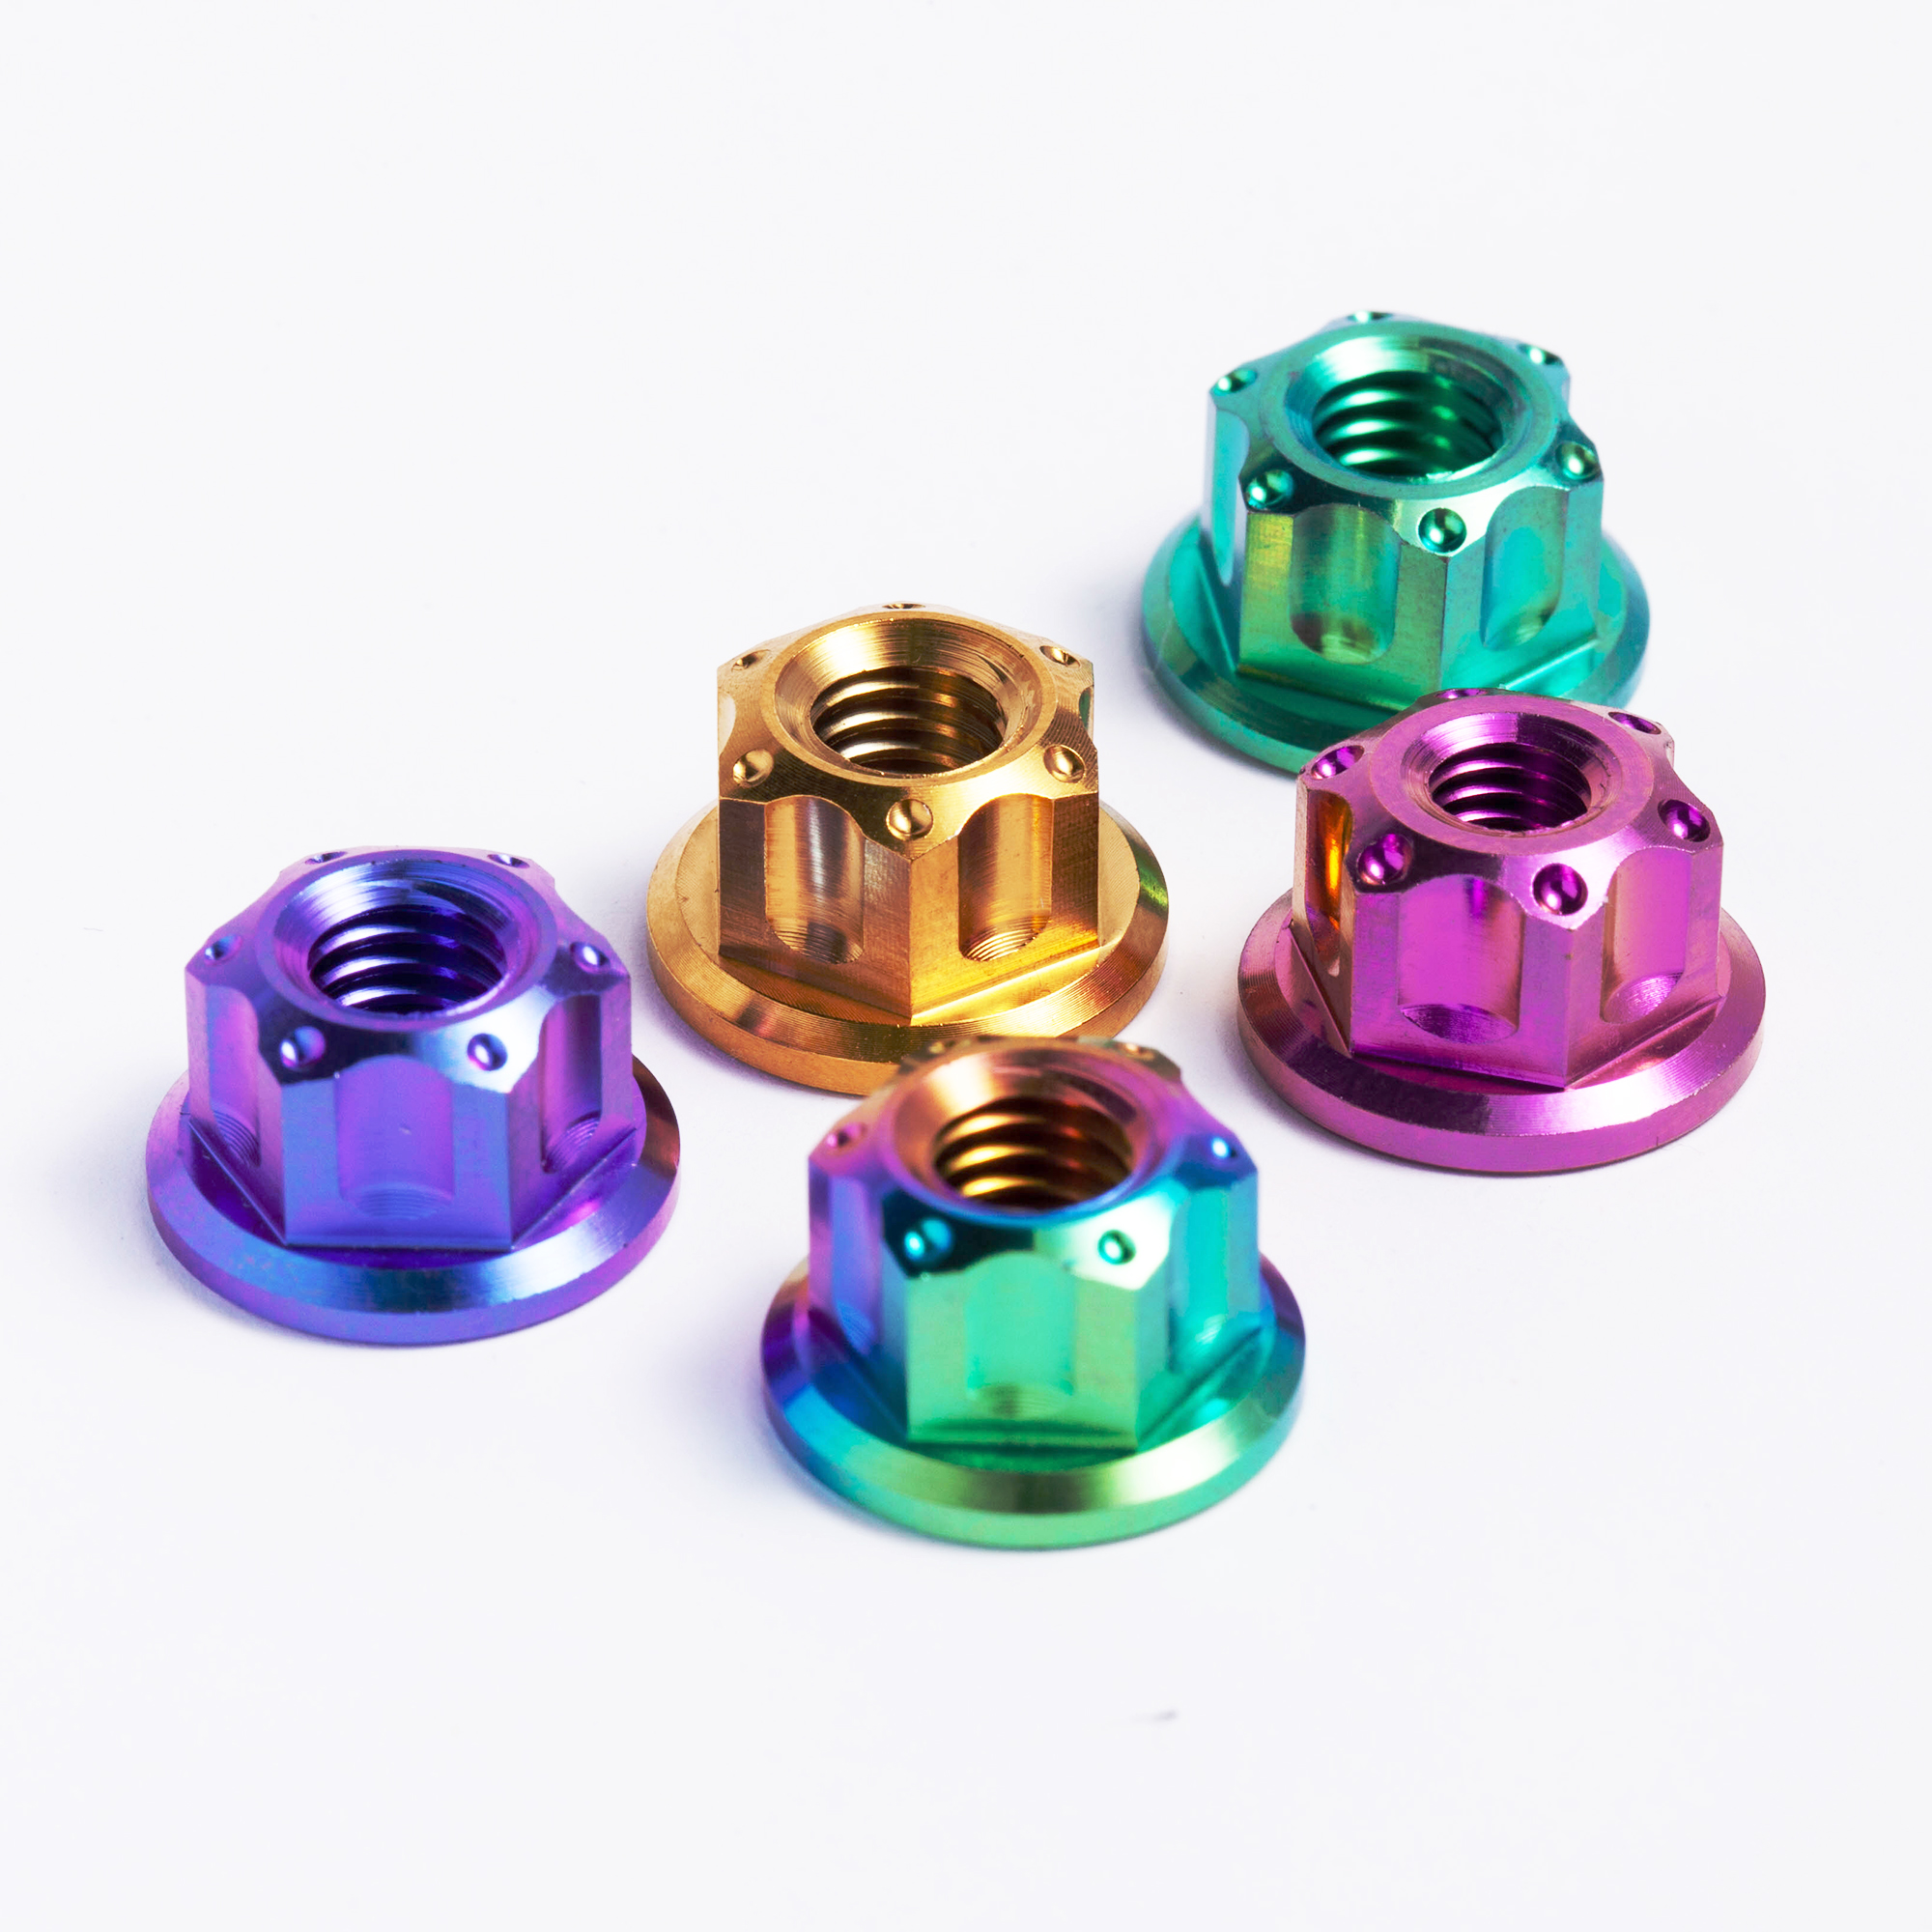
BST-TI MC-NUT-03 Titanium GR5 Self-Locking Hex Flanged Lug Lock Nuts
Explore Product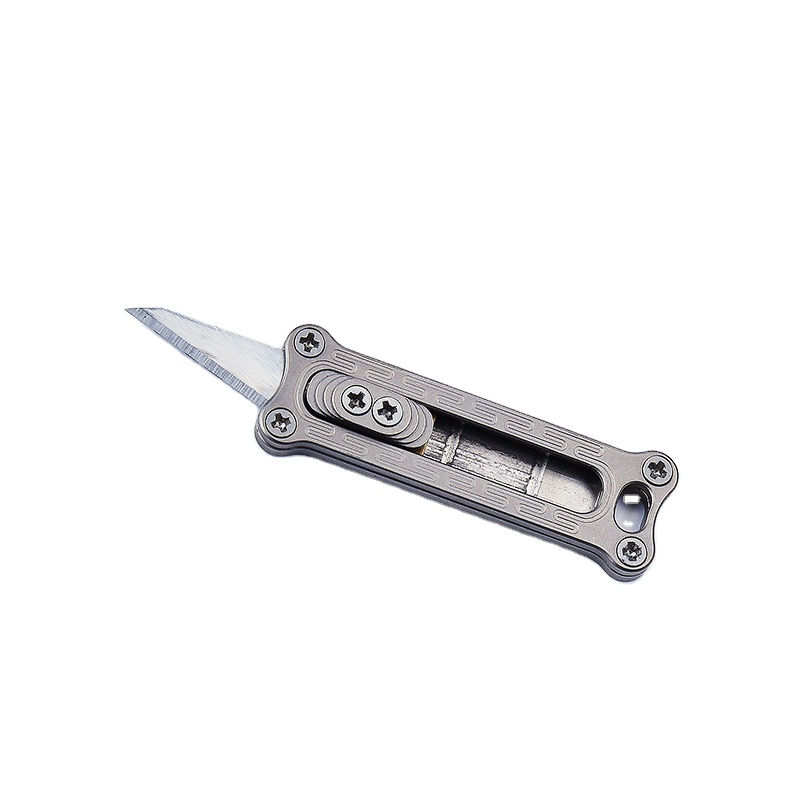
BST-TI Titanium Alloy EDC Pocket Precision Multi-Tool System
Explore Product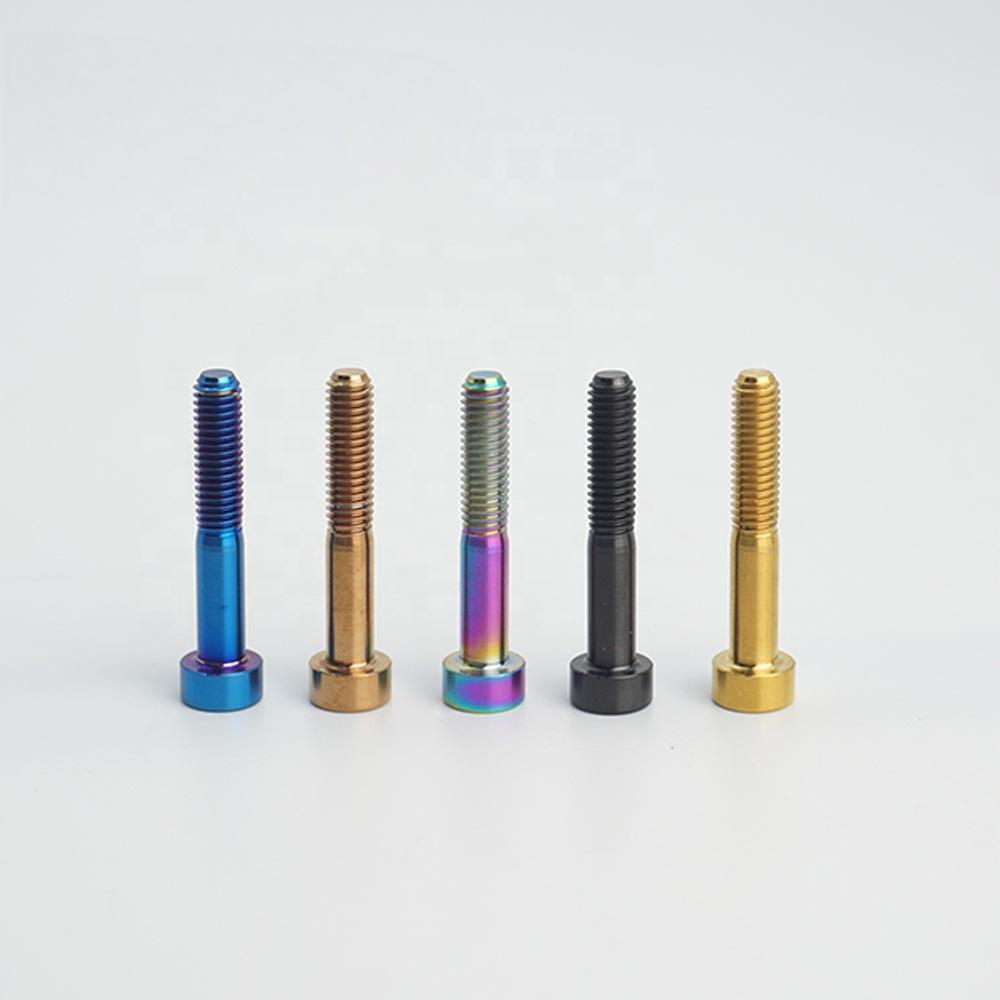
Titanium CNC Bolts Hex Button Head Black Oxide Finish Rustproof M5 M6
Explore ProductEngineering Whitepaper: Valvetrain Dynamics & Titanium Metallurgy
Why switching to Grade 5 Ti-6Al-4V valve retainers eliminates valve float, enhances thermal fatigue limits, and elevates engine RPM thresholds.
Inertia Reduction & Valve Float Control
In high-revving internal combustion engines, valvetrain inertia is the limiting factor for engine speed. Valve retainers reciprocating at over 8,000 RPM create massive dynamic loads. By reducing retainer mass by up to 45% compared to conventional 4140 chromoly steel, Wexra's Ti-6Al-4V retainers significantly drop reciprocating mass, preventing destructive harmonic valve float without demanding excessive spring seat pressure that increases cam lobe wear.
Metallurgical Integrity: Grade 5 Ti-6Al-4V
Our valve retainers are precision-turned exclusively from certified aerospace-grade Ti-6Al-4V (Grade 5). With an alpha-beta crystal structure achieved through controlled vacuum annealing, the alloy delivers a minimum tensile strength of 895 MPa, exceptional fatigue resistance under billions of stress cycles, and low thermal conductivity that helps keep excessive exhaust valve stem heat from degrading the spring temper.
PVD & Anodized Wear Protection
Titanium in raw contact with hardened steel valve keepers can be prone to micro-fretting or galling under extreme vibrations. Wexra addresses this through precision multi-axis CNC surface profiling and specialized surface treatments, including hard physical vapor deposition (PVD) and controlled micro-arc oxidation, ensuring the retainer tapers lock securely with 7-degree, 8-degree, or 10-degree keepers under high spring loads.
| Mechanical / Thermal Metric | Wexra Gr5 Titanium (Ti-6Al-4V) | Standard 4140 Chromoly Steel | 6061-T6 Billet Aluminum | Impact on Valvetrain Dynamics |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 | 7.85 | 2.70 | 44% mass reduction vs steel; eliminates valve float |
| Yield Strength (MPa) | 828 | 655 | 276 | Withstands extreme open spring loads over 400 lbs |
| Tensile Strength (MPa) | 895 - 1000 | 850 - 1020 | 310 | Zero deformation under cyclic shock impact |
| Fatigue Limit (10⁷ cycles) | 510 MPa | 420 MPa | 96 MPa | Long-term durability in endurance competition |
| Corrosion & Acid Resistance | Immune (Native TiO₂) | Vulnerable (Oxidizes) | Moderate (Pitting prone) | Impervious to ethanol, methanol, & acidic fuel gases |
Localized Engineering Scenarios in the Grodno Market
Strategically positioned at the western logistics and industrial crossroads of Belarus, the Grodno region demands hardware engineered for severe operational realities.
Cross-Border Fleet Heavy Duty & Transport Hubs
Grodno's proximity to the EU border makes it a critical logistical transfer zone. Commercial turbo-diesel engines hauling heavy transit loads frequently encounter severe cylinder head thermal gradients. Custom-engineered titanium retainers and high-strength Grade 5 valvetrain fasteners provide commercial transport rebuilders with insurance against catastrophic valve dropper failures during extended intercontinental hauls.
Agrotechnical & Heavy Agricultural Machinery
Grodno's fertile agricultural basin relies on high-torque combines, tractors, and processing gear running non-stop during harvest windows. Valve failure in seasonal harvesting engines causes critical downtime. Wexra's CE-certified titanium components resist the aggressive nitric-acidic byproducts found in modern high-blend bio-diesel, ensuring valve seats remain concentric across extreme operational duty cycles.
Autocross, Drag & Regional Motorsport Tuning
The active regional motorsport and tuning culture around Grodno requires bespoke engine building. Whether modifying 4-cylinder turbocharged Japanese imports or European straight-six powerplants, tuners trust Wexra’s custom-engineered retainers to safely push cam profiles past 300° duration and unlock redlines exceeding 9,000 RPM without valve-to-piston interference.
Procurement & Technological Trends in Grodno (2025–2030)
Analyzing key structural shifts in industrial supply chains and precision components across regional engine rebuilders.
Supply Chain De-risking & Direct Factory Sourcing
Industrial procurement teams in Grodno are moving away from multi-tier intermediaries. By connecting directly with ISO 9001:2015 certified manufacturers like Wexra Titanium, workshops eliminate middleman markups, gain access to verifiable Mill Test Certificates (MTC), and secure customized production runs backed by international regulatory documentation.
Alternative Fuel Valvetrain Adaptations
The rapid regional expansion of Compressed Natural Gas (CNG) and Liquefied Petroleum Gas (LPG) engine conversions creates extreme combustion chamber temperatures. Gaseous fuels lack the lubricity of liquid gasoline. Titanium valvetrain components, when paired with appropriate PVD coatings, provide the thermal stability needed to prevent micro-welding at the keeper interface.
Stringent Compliance & Material Traceability
Quality assurance standards across the Eurasian transport sector increasingly mandate full CE certification, RoHS compliance, and chemical spectrometry verification. Wexra provides complete batch traceability on every valve retainer run, guaranteeing exact 6% Aluminum and 4% Vanadium composition without harmful interstitial impurities.
Factory Advantages & Manufacturing Excellence
Jiaxing Wexra Titanium Products Co., Ltd. combines advanced CNC multi-axis machining with rigorous metallurgical control.
Certified Quality Systems (ISO 9001:2015)
Every step of our process—from titanium raw billet inspection through turning, thread rolling, anodizing, and final optical CMM measurement—adheres to strict ISO 9001:2015 protocols. Our products hold full CE certification, UKCA compliance, and RoHS/REACH chemical safety validations.
Sub-Micron Precision CNC Machining
Titanium requires rigid machine setups, dedicated tool coatings, and optimized feeds to prevent work hardening. Our factory utilizes multi-axis CNC turning centers to machine complex valve retainer taper geometries with repeatable tolerances down to ±0.01 mm, guaranteeing a perfect taper lock fit.
OEM & Custom Drawing Specialization
Whether you need standard dual-spring retainers, beehive spring profiles, or custom step heights for non-standard valve installed heights, our technical team turns your CAD drawings, STEP files, or physical samples into production-ready components within days.
Frequently Asked Questions: Grodno Procurement & Engineering
Detailed technical answers for regional automotive technicians, wholesale distributors, and machine shop buyers.
Why choose Grade 5 (Ti-6Al-4V) instead of Grade 2 for valve retainers?
Grade 2 titanium is commercially pure with a tensile strength of around 345 MPa, which is insufficient for the dynamic shock loads of high-lift engine valvetrains. Grade 5 is an engineered alpha-beta alloy yielding over 895 MPa tensile strength, providing the structural stiffness required to prevent keeper pull-through under heavy spring loads.
What CE documentation and test reports accompany shipments to Grodno?
Every commercial export is supplied with complete EN 10204 Type 3.1 Mill Test Certificates (MTC), optical coordinate measuring machine (CMM) dimensional reports, RoHS compliance certifications, and CE conformity documentation to ensure seamless clearance and strict workshop compliance.
Can Wexra produce custom retainers from physical samples or CAD files?
Yes. Our engineering division routinely works from 2D blueprints (PDF/DWG), 3D parametric files (STEP/IGES), or worn physical samples. We provide full Design for Manufacturability (DFM) reviews to verify keeper taper angles, spring step diameters, and clearance before batch CNC production begins.
How does titanium retainer wear compare to steel over extended engine life?
When properly installed with compatible valve keepers and spring seats, Grade 5 titanium retainers provide service lives exceeding hundreds of thousands of kilometers. For extreme high-lift racing setups, we offer specialized micro-arc oxidation and PVD wear coatings to eliminate fretting.
What are the typical lead times and minimum order quantities (MOQ)?
Standard catalog profiles are maintained in stock for immediate dispatch. Custom OEM prototyping runs typically ship within 10 to 14 business days, with flexible production runs structured to accommodate specialized race shops as well as high-volume distributor supply chains.
How do titanium retainers interact with dual vs. beehive valve springs?
Wexra designs retainers specifically matched to your spring architecture. For dual springs, we machine concentric inner and outer locating steps to prevent spring walk. For modern beehive springs, our ultra-compact retainer profile minimizes top-end mass while maintaining critical keeper contact area.
Ready to Upgrade Your Valvetrain Reliability in Grodno?
Connect with Wexra Titanium’s engineering support team today. Request a custom quote, technical consultation, or complete CE & material test portfolio.