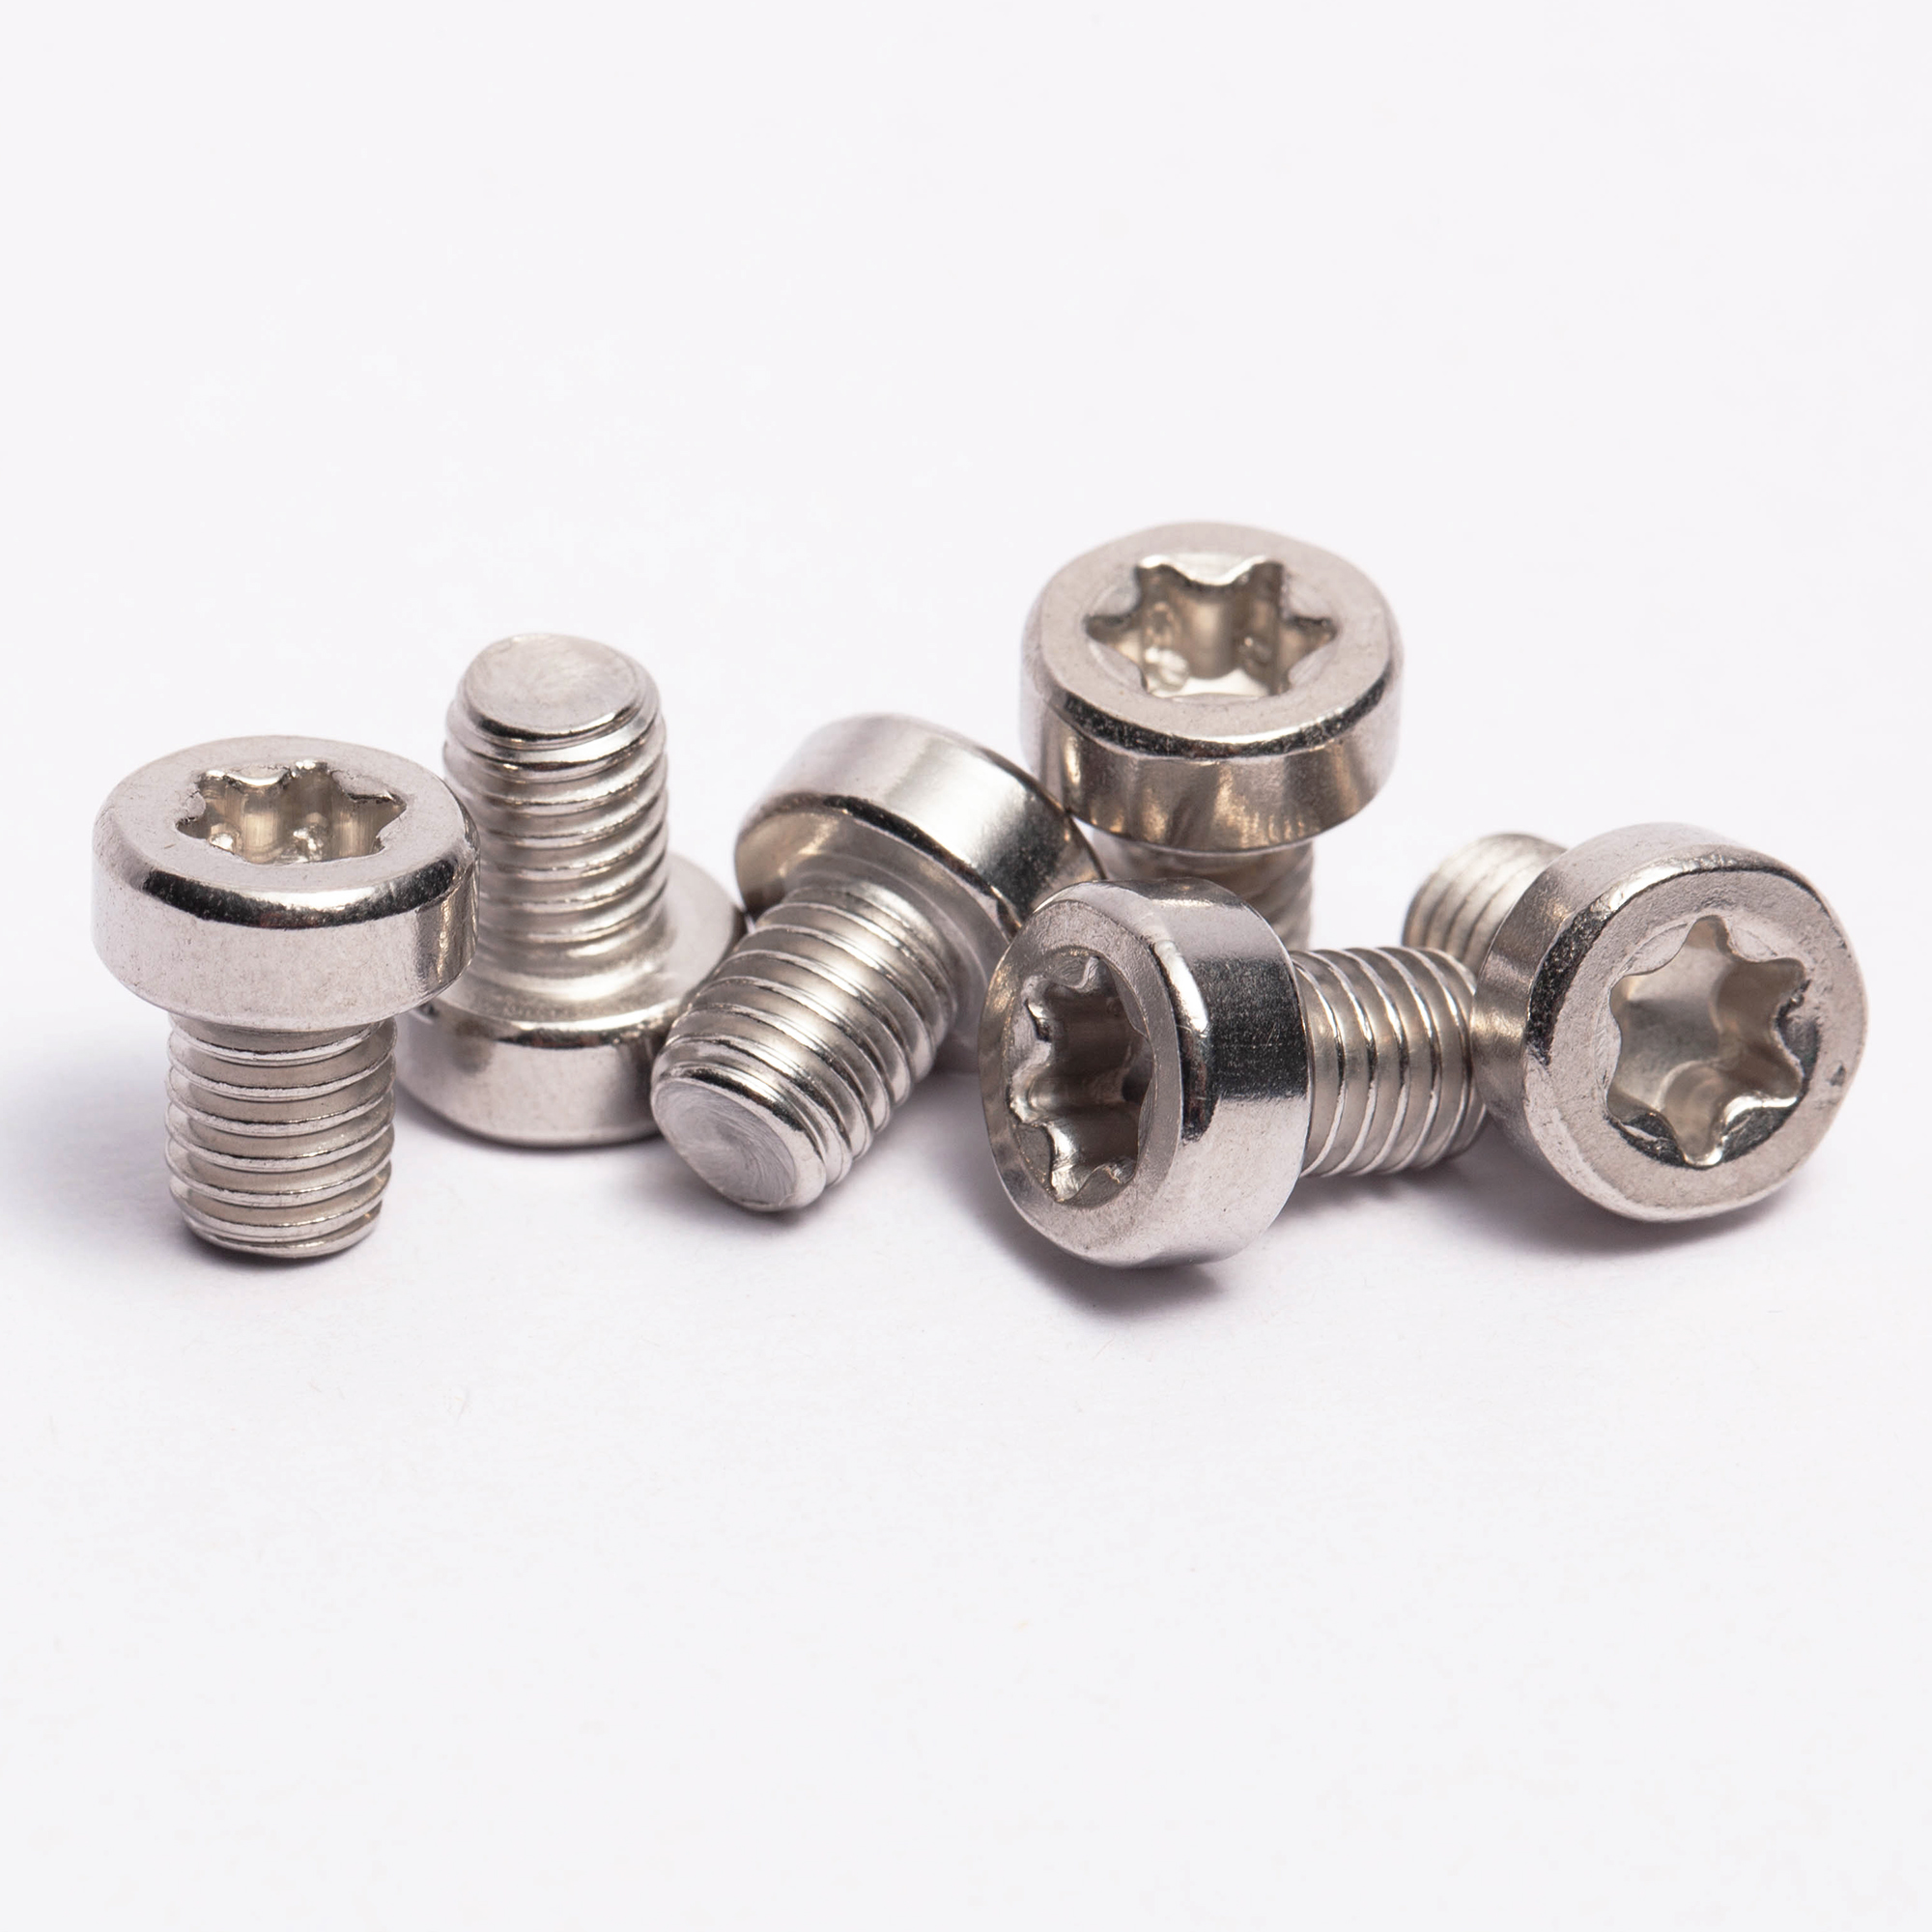
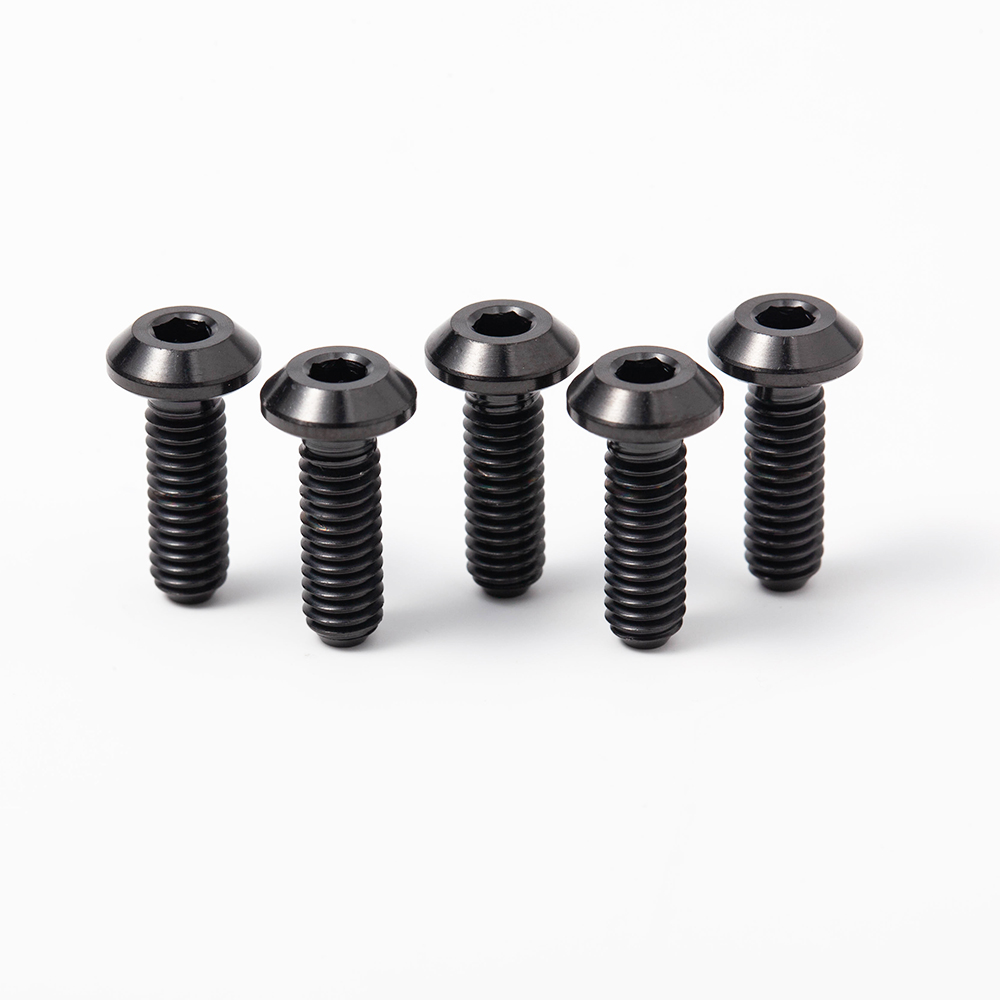
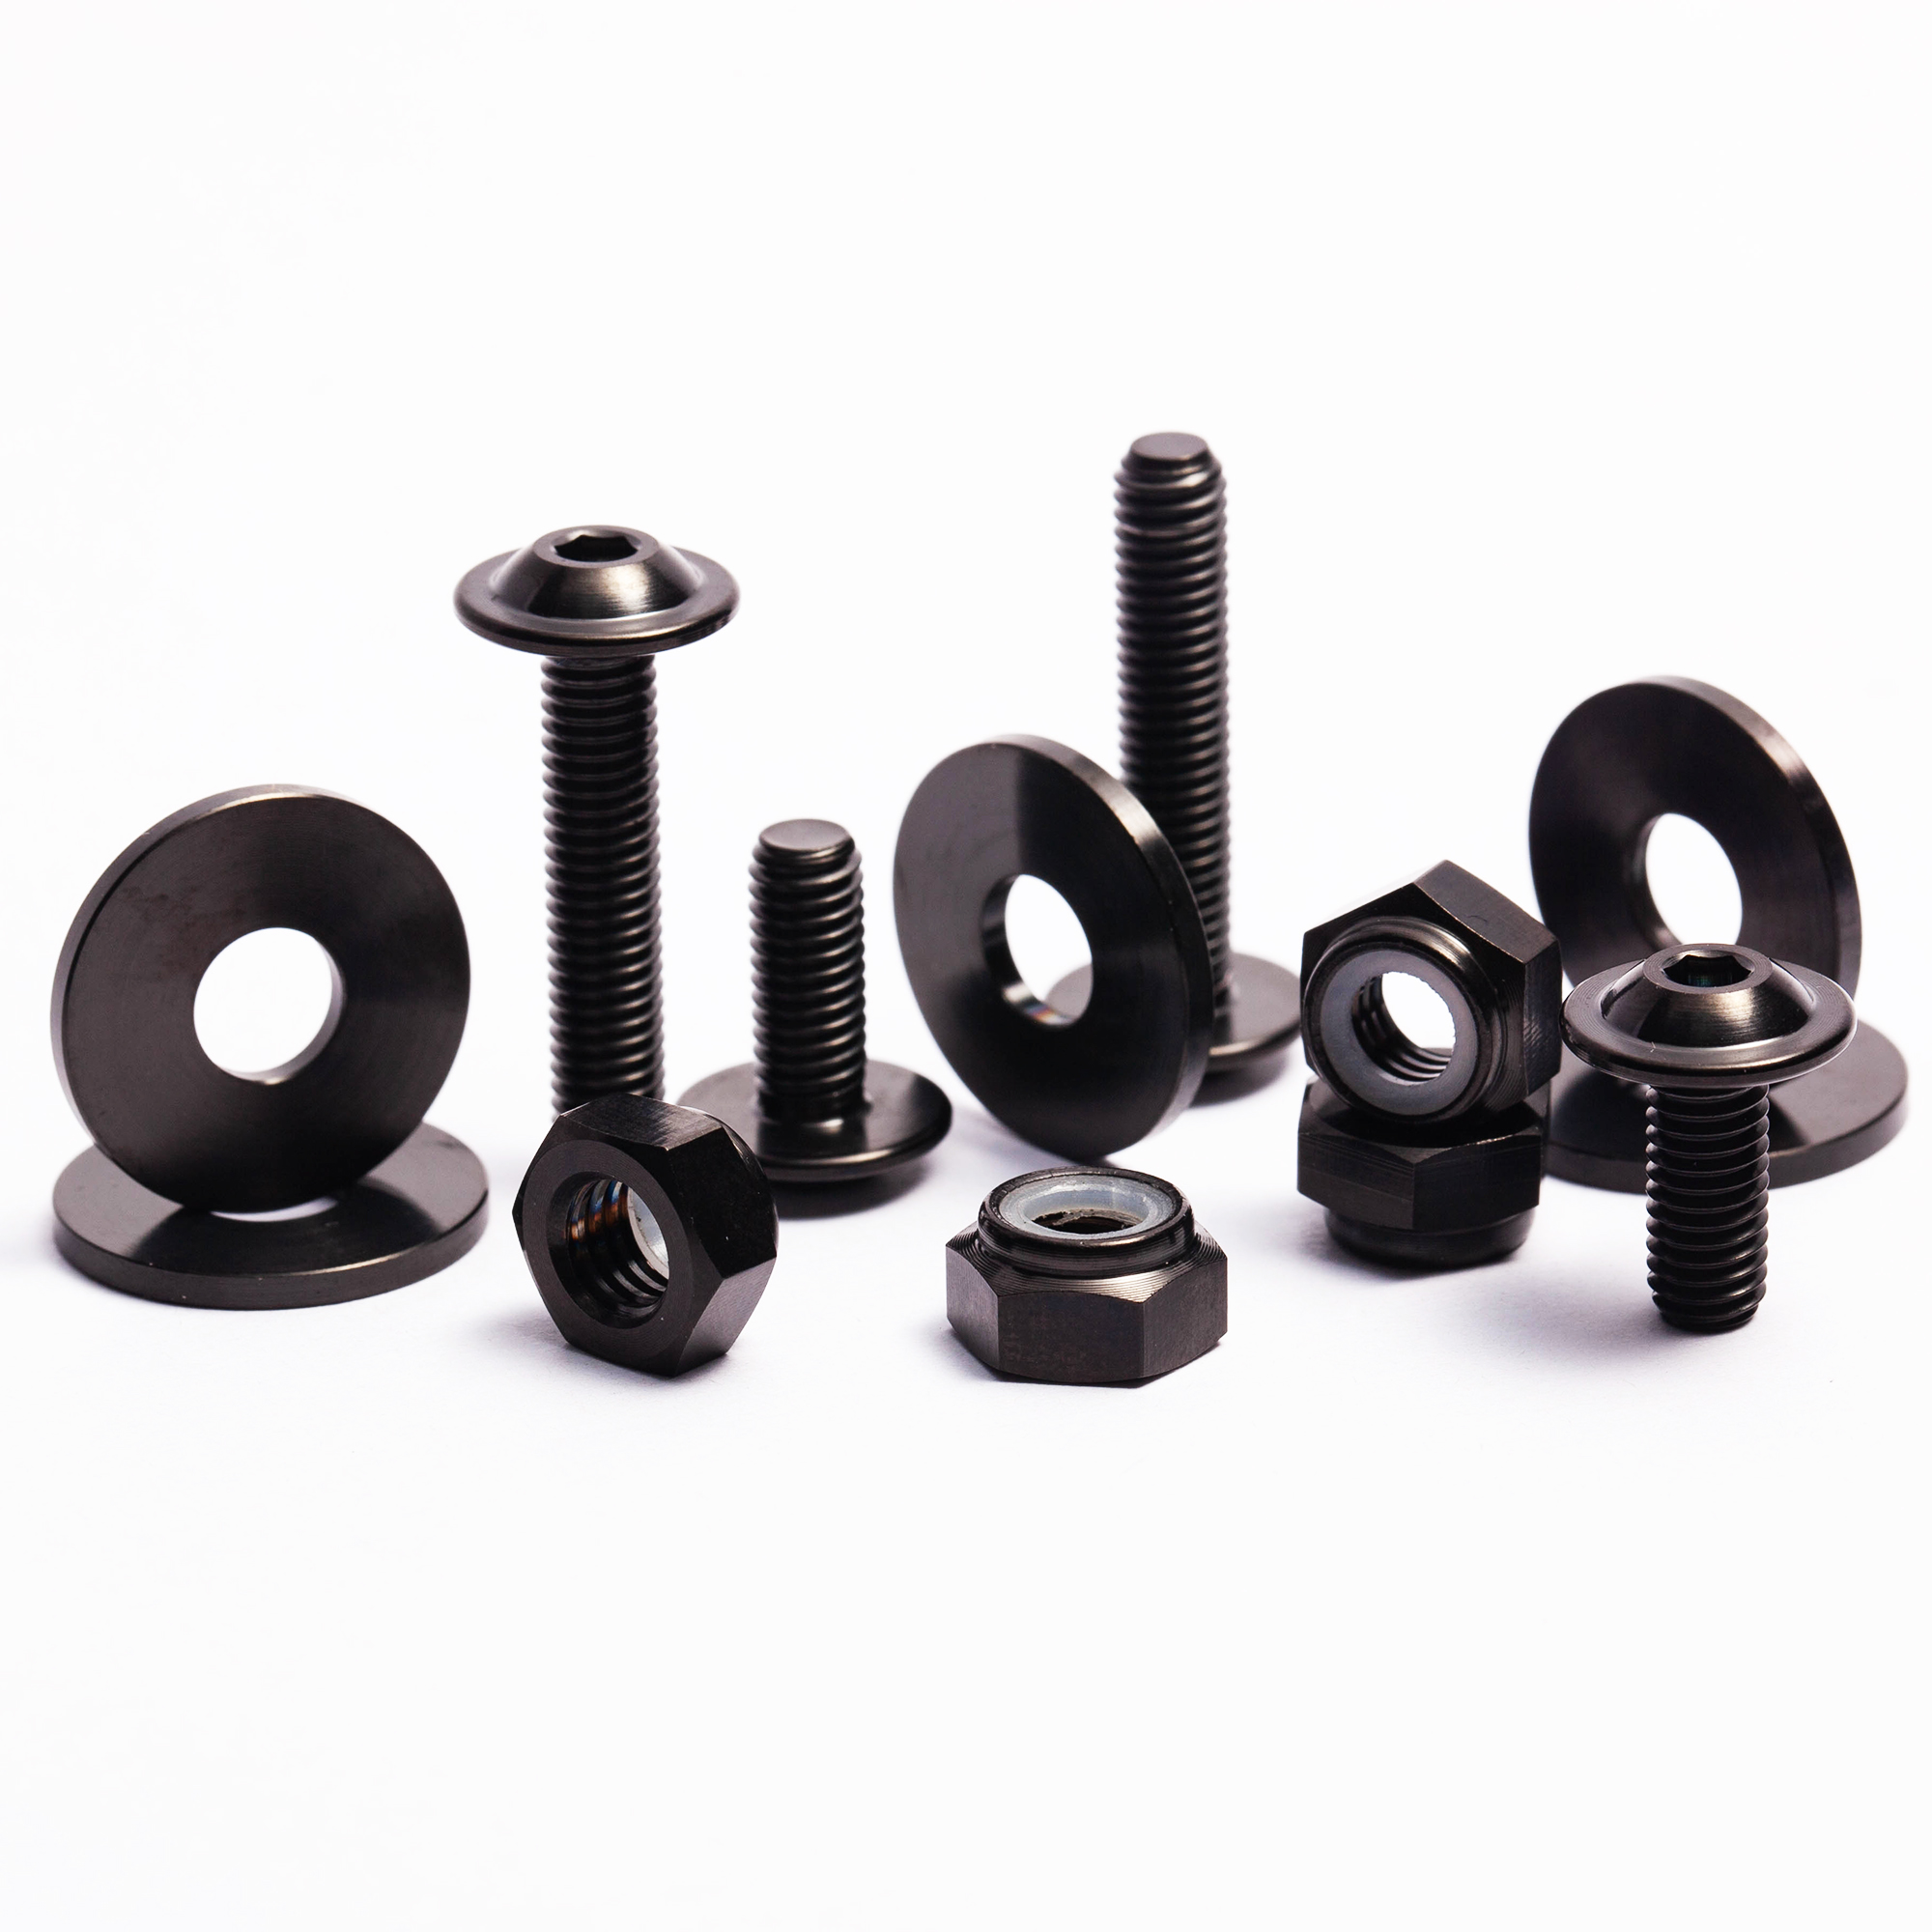
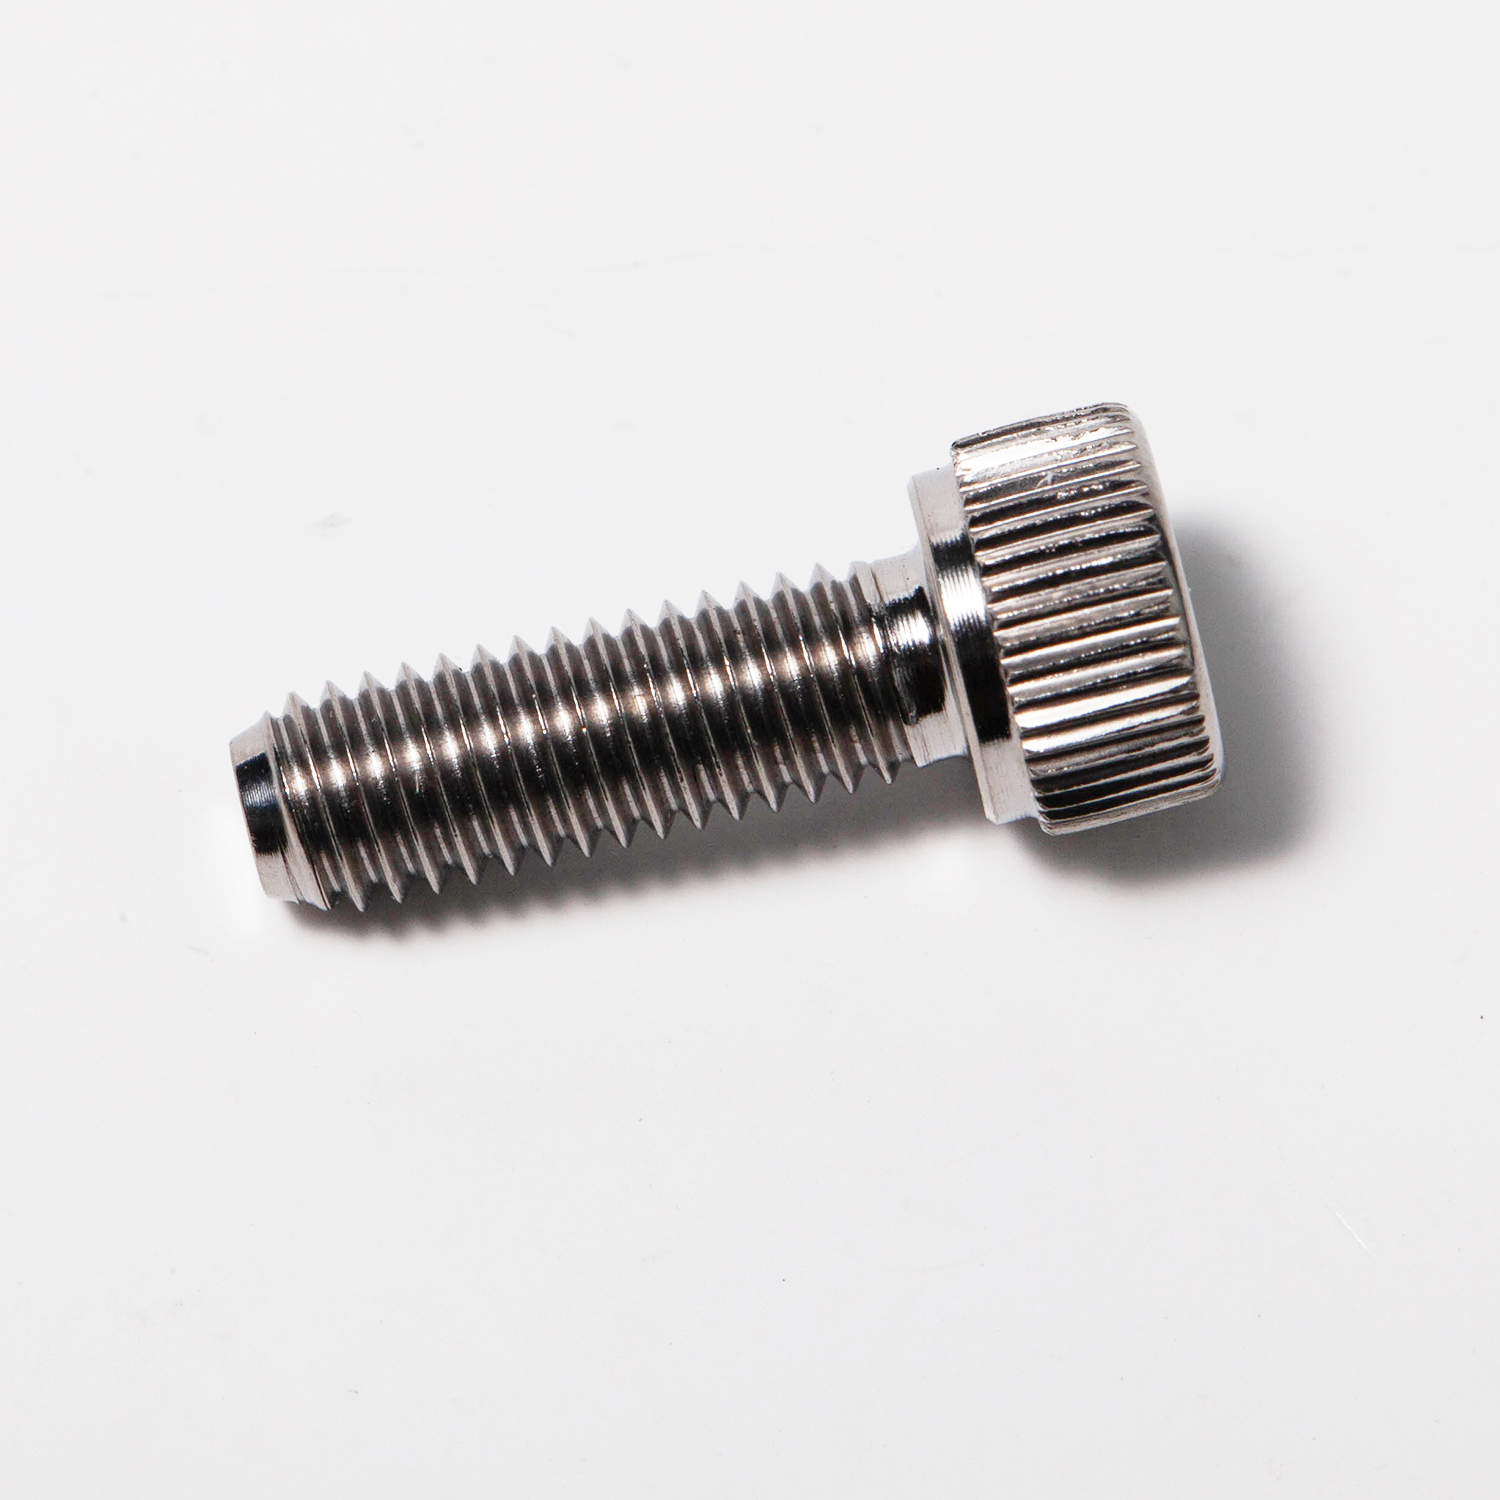
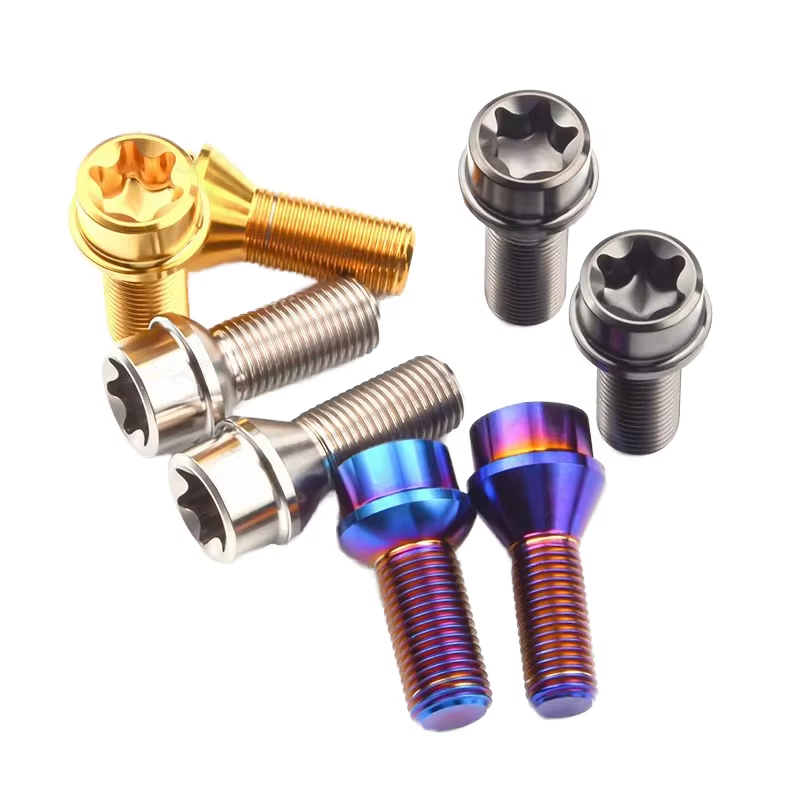
Precision-machined fasteners engineered for high-stress clamping, corrosive chemical exposure, and unsprung rotational weight reduction across automotive, motorcycle, and cycle assemblies.
As the historical cradle of British metalworking, Birmingham and the wider West Midlands automotive corridor rely heavily on precision fasteners that bridge aerospace performance with automotive production cycles.
Situated within proximity to the UK "Motorsport Valley" (Silverstone cluster and Solihull automotive prototyping plants), engineering teams procure titanium fasteners to strip reciprocating weight in valvetrains, brake systems, and unsprung suspension hubs.
Proximity to regional fluid power systems and coastal transport corridors demands materials that withstand aggressive road salts, de-icers, and saltwater galvanic exposure where conventional 8.8 and 10.9 zinc-plated carbon steel bolts rapidly rust.
Local tier-1 aerospace machine shops operating under strict AS9100/ISO frameworks impose rigorous requirements on imported hardware, mandating EN 10204 3.1 Mill Test Certificates (MTC), ultrasonic testing, and zero-defect thread pitch accuracy.
An objective comparison of primary manufacturers and premier UK stocking distributors delivering Gr2, Gr5 (Ti-6Al-4V), and custom surface-treated titanium fasteners to West Midlands engineering operations.
HQ / Export Profile: Direct Manufacturer (Jiaxing, China) servicing UK, DE, and US markets under strict ISO 9001:2015 frameworks.
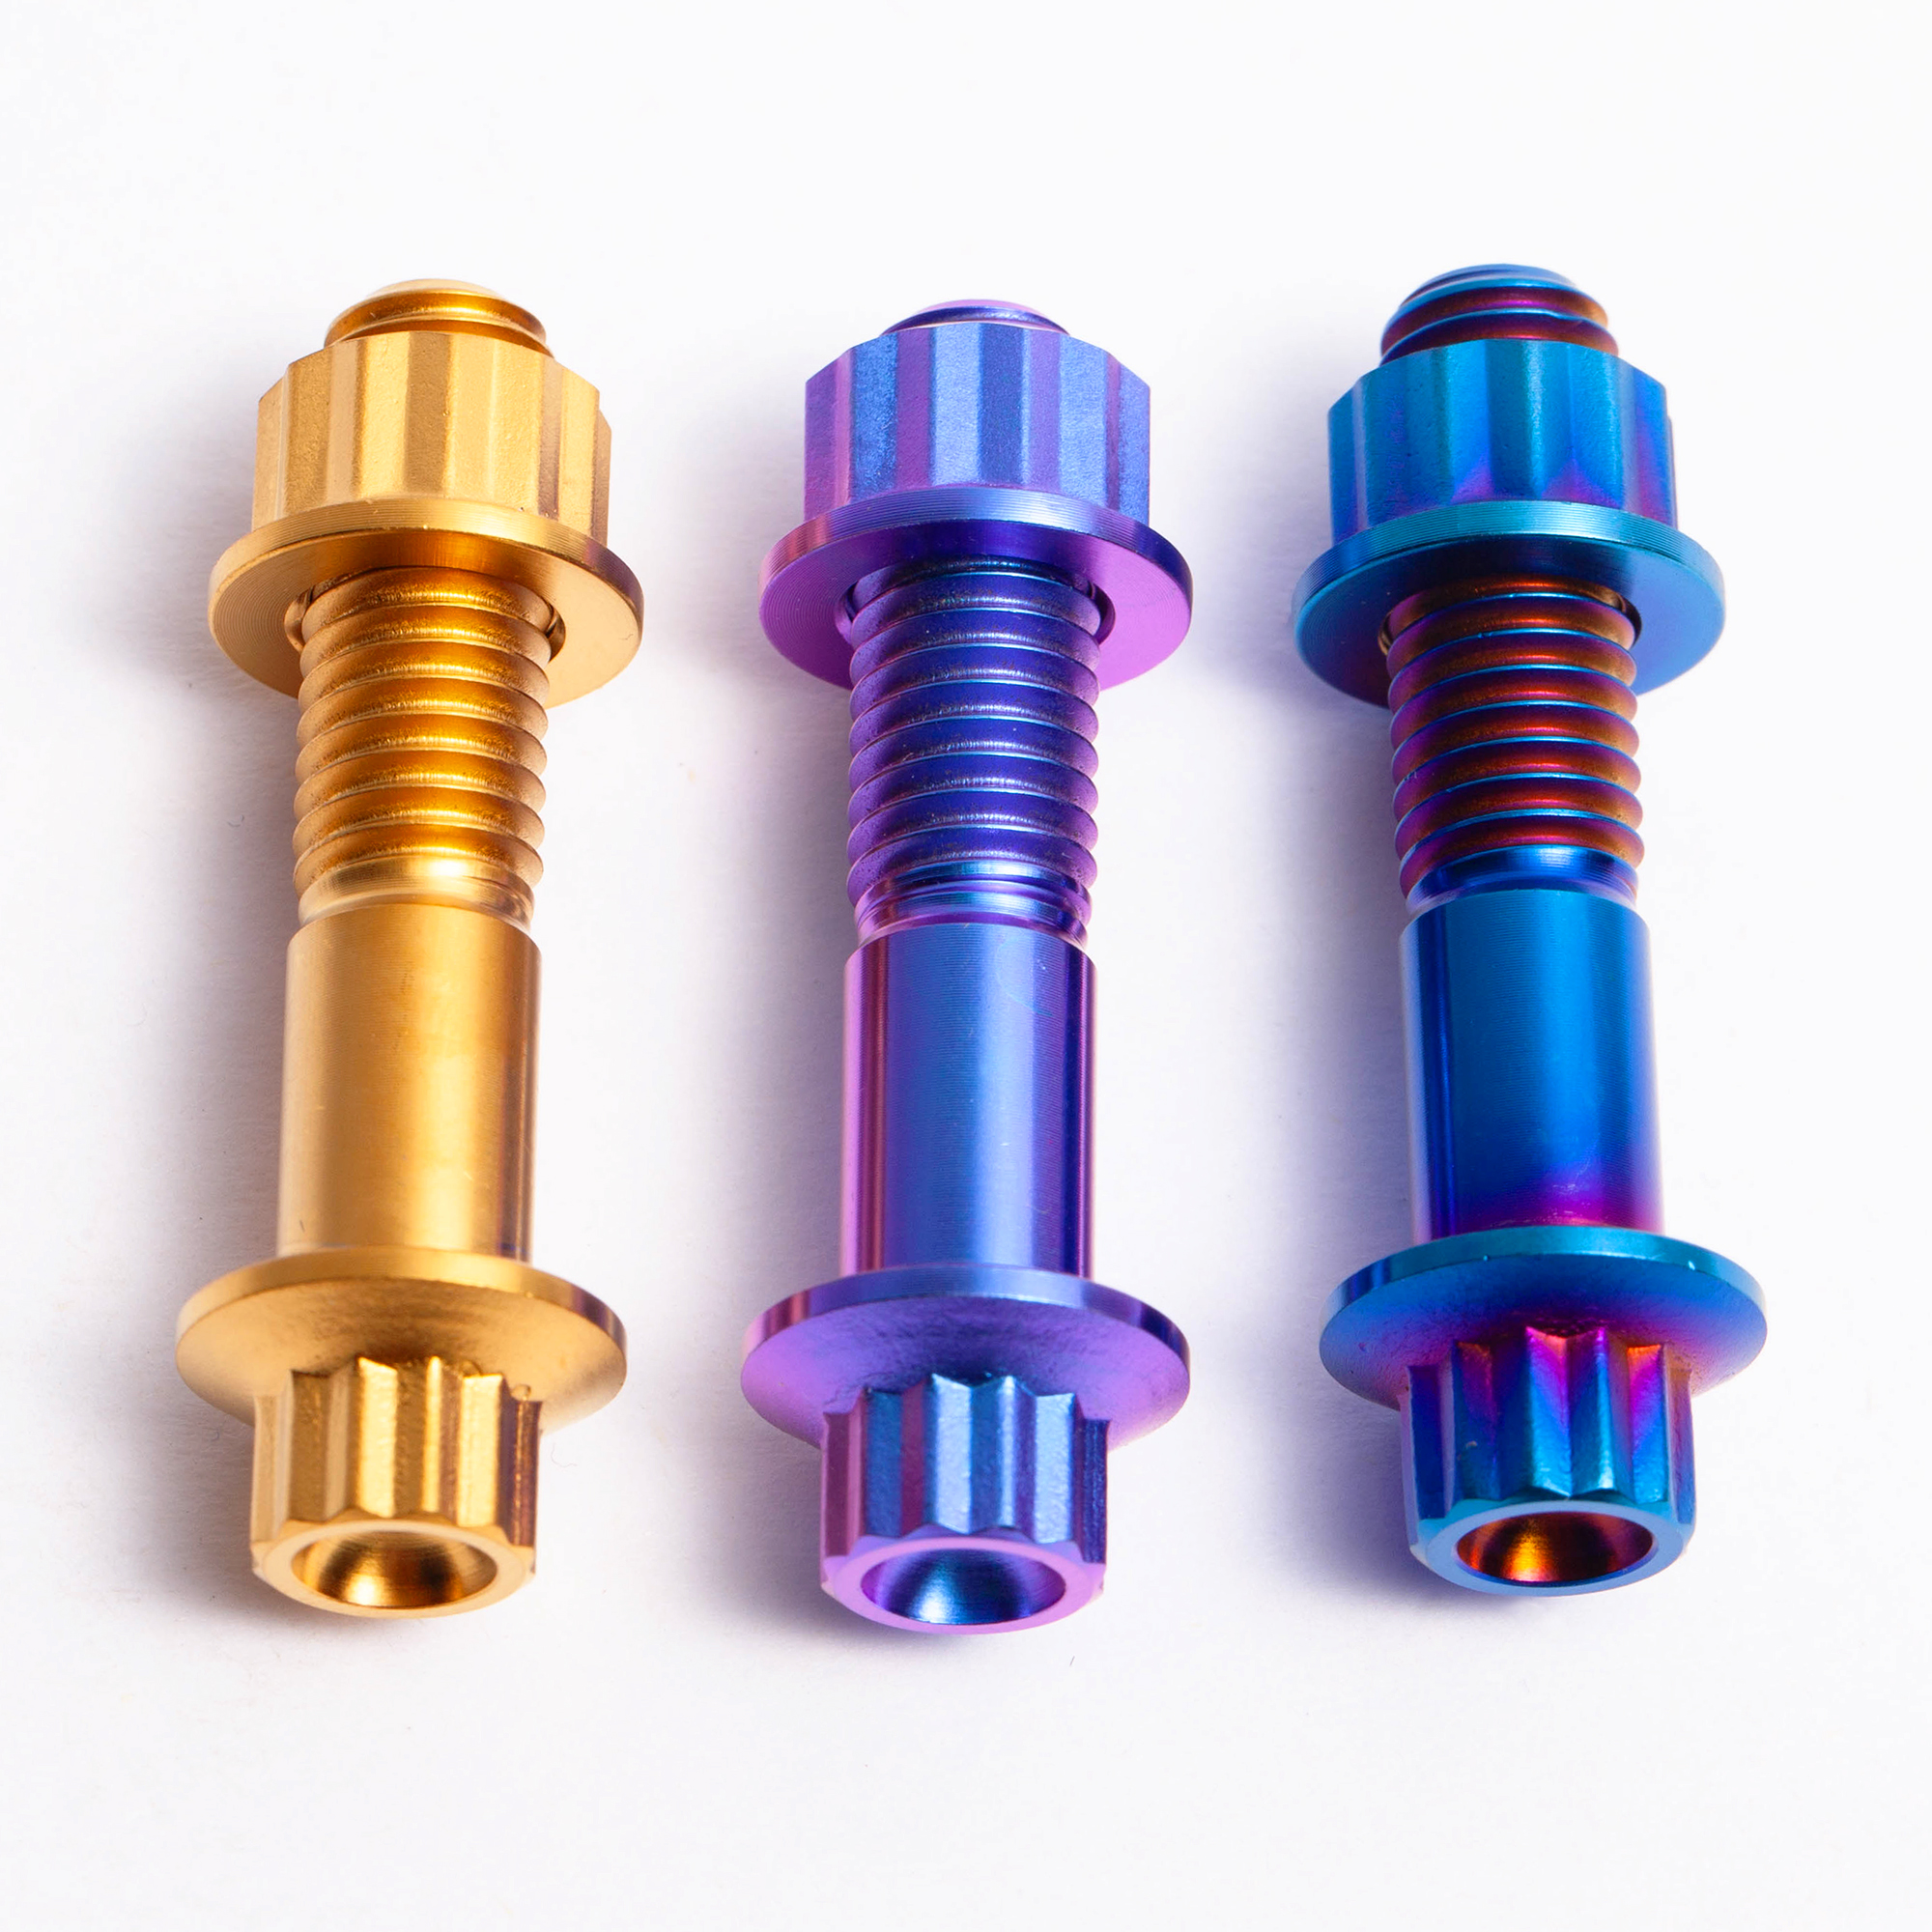
Specialization: Full OEM/ODM custom CNC turning, rolled threads, and electrolytic color anodizing (Gold, Violet, Burnt Blue) plus PVD Titanium Nitride (TiN).
Competitive Edge: Direct factory pricing, mill-certified Grade 5 raw materials, ±0.01mm tolerance capabilities, and dedicated technical support for British custom engineering designs.
HQ: Gloucestershire, UK.
Specialization: Internationally renowned supplier of racing motorcycle and automotive titanium fasteners, offering rolled threads in natural polished and high-end gold anodized finishes.
Regional Utility: Rapid stock availability for trackside teams across Castle Combe, Donington, and Birmingham tuning workshops.
HQ: Stourbridge, West Midlands.
Specialization: High-tensile structural hardware, special exotic alloys, and custom fasteners servicing general manufacturing and rail infrastructure across Greater Birmingham.
Regional Utility: Fast same-day local distribution and blanket stock-holding agreements for industrial repair facilities.
HQ: Bilston, West Midlands.
Specialization: Corrosion-resistant components, duplex stainless steel, and titanium alloy sourcing for architectural, marine, and commercial machinery applications.
Regional Utility: Massive inventory footprint in the Black Country corridor with extensive UK distribution capabilities.
HQ: Cradley Heath, West Midlands.
Specialization: Bespoke non-standard turned parts, metric and imperial threading in high-performance materials including titanium, Inconel, and brass.
Regional Utility: Rapid prototyping and replacement runs for historical automotive, defense, and power generation rebuilds.
HQ: Nationwide UK Distribution.
Specialization: Focuses purely on high-grade titanium fasteners for mountain bikes (MTB), performance cycling, and clubman track racers.
Regional Utility: Direct-to-consumer and bike shop distribution across the Birmingham cycle courier and competition cycling sectors.
HQ: Shropshire, UK.
Specialization: Precision manufactured fasteners, colored titanium hardware, metric fine conversion studs, and laser-marked specialty bolts.
Regional Utility: Serving small-batch artisanal automotive fabricators and independent motorsport builders throughout the Midlands.
HQ: Birmingham, UK.
Specialization: Heavy industrial, petrochemical, and pressure-vessel studs manufactured to ASTM specifications with full 3.1 material traceability.
Regional Utility: High compliance documentation for chemical processing tanks and heat exchangers in Midlands processing plants.
HQ: Warwickshire, UK.
Specialization: High-end Grade 5 titanium bolts tailored for automotive engine bays, titanium wheel bolts, and titanium exhaust manifold hardware.
Regional Utility: Close technical ties with luxury vehicle tuners and sports car restoration hubs around Coventry and Solihull.
HQ: Direct Factory Global Operations.
Specialization: High-volume factory runs, scalable prototype-to-mass manufacturing, custom anodized cosmetic lines, and bulk wholesale distribution directly to Birmingham warehouse depots.
Regional Utility: Removes secondary distributor markups, allowing UK OEMs to source bespoke gold titanium hardware at direct-from-foundry prices.
Understanding the structural differences between Commercially Pure Grade 2, Aerospace Grade 5 (Ti-6Al-4V), and standard automotive steel hardware.
| Material Specification | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Corrosion Mechanism | Recommended Torque Strategy |
|---|---|---|---|---|---|
| Titanium Gr5 (Ti-6Al-4V) | 4.43 | ≥ 895 | ≥ 828 | Inert Stable Oxide | Standard with anti-seize (~85% steel torque) |
| Titanium Gr2 (Pure CP) | 4.51 | ≥ 345 | ≥ 275 | Superior Chemical | Low clamping applications only |
| Stainless Steel 316 (A4-70) | 8.00 | 700 | 450 | Passive Film | Prone to galling without lubrication |
| High Tensile Steel Class 10.9 | 7.85 | 1040 | 940 | Sacrificial Zinc/Rust | Standard engineering torque table |
An electrochemical process that thickens the natural titanium oxide (TiO&sub2;) layer. Through light refraction interference, precise voltages generate deep golden hues without altering thread pitch dimensions (<0.1μm variance).
Physical Vapor Deposition (PVD) produces an ultra-hard ceramic surface layer (approx. 2000-2500 HV). TiN provides exceptional abrasion resistance, making it ideal for repeatedly torqued wheel studs and track day caliper bolts.
Because titanium has a low thermal conductivity, friction heat can cause thread microwelding (galling). We supply rolled threads instead of cut threads, combined with copper-slip or molybdenum disulfide anti-seize paste for lifetime reliability.
From competitive racing paddocks to precision medical apparatus, gold titanium screws serve critical structural and aesthetic functions.
Track racing teams across Donington and Mallory Park utilize M8 and M10 gold titanium flange bolts to secure front brake calipers and rear drive sprockets, resisting intense braking heat cycles.
Tuning shops in Solihull and Coventry replace dreary zinc bolts with M6 gold anodized dress-up washers and cap screws across valve covers, intercooler piping, and strut towers.
Birmingham commuters and regional cycling racers fit countersunk M5/M6 stem, disc rotor, and water bottle cage bolts, ensuring zero surface corrosion through winter road salt spray.
Medical tooling and non-magnetic instrumentation manufacturing in the Edgbaston technology belt rely on Gr2/Gr5 titanium fasteners due to their total non-magnetic and biocompatible profile.
Analyzing industry transitions toward EV lightweighting, circular material lifecycles, and high-precision CNC manufacturing standards.
With major UK automotive manufacturing transitioning to electric architectures in the Midlands, high-voltage battery enclosures and structural subframes require titanium's high strength-to-weight ratio to offset excessive battery pack curb weight without compromising crash load performance.
Unlike hexavalent chrome and toxic electroplating processes historically used on carbon steel, electrolytic titanium anodizing is inherently cleaner, requiring no toxic heavy metal baths. This aligns directly with strict UK REACH regulations and regional net-zero corporate initiatives.
Modern procurement standards reject screw fasteners with machine-cut threads for load-bearing duties. Cold thread rolling reorients the metal grain structure parallel to thread profiles, improving fatigue resistance by up to 30% under cyclic vibrational stress.
Expert metallurgical answers addressing torque, galling, certifications, and international logistics.
Yes, in the vast majority of applications. Grade 5 (Ti-6Al-4V) features a minimum tensile strength of 895 MPa and yield strength of ~828 MPa, which closely approaches Class 10.9 steel (1040 MPa tensile). However, because titanium has roughly half the modulus of elasticity of steel (~114 GPa vs ~210 GPa), titanium fasteners stretch more under equivalent loads, delivering superior resistance to vibrational loosening while requiring appropriate torque calibration.
Unlike paint or powder coating, electrolytic anodization does not add an external pigment layer; it microscopically thickens the natural titanium oxide surface film to refract light at the gold spectrum. The dimensional growth is negligible (<0.0001 mm), meaning standard ISO metric and UNF class 6g thread fits remain completely unaffected. It cannot chip or flake off, though abrasive friction under high torque should be protected with an anti-seize paste or PVD TiN coating.
Every industrial order is backed by comprehensive ISO 9001:2015 traceability. We supply EN 10204 Type 3.1 Mill Test Certificates (MTC) stating chemical composition (Ti, Al, V, Fe, C, N, H, O) and mechanical tensile data, alongside optical coordinate dimensional inspection reports and full UKCA/RoHS/REACH chemical compliance declarations.
Galling occurs when friction removes the protective oxide layer, causing raw metal surfaces to bond. For titanium-into-aluminum or titanium-into-titanium threads, always apply an anti-seize lubricant (such as nickel-based, copper-based, or synthetic PTFE assembly grease) and reduce dry installation torque by approximately 15% to 20% to achieve the intended clamping pre-load.
For in-stock catalog hardware, air express couriers (DHL/FedEx/UPS) deliver to West Midlands addresses within 4 to 6 business days with complete customs handling. Custom CNC runs and bulk OEM volume shipments are scheduled across a 15 to 25 day manufacturing timeline followed by express air cargo or consolidated sea freight into the Port of Felixstowe or Southampton.
Equipped with state-of-the-art CNC turning centers, multi-axis milling, precision thread rolling machines, and proprietary surface anodizing systems.
Operating dedicated titanium multi-axis turning and milling equipment yielding tolerances down to ±0.01 mm, maintaining exact concentricity and broached socket integrity for Torx and Hex drive heads.
Our quality assurance protocol governs every manufacturing phase: starting with spectroscopic chemical verification of virgin titanium billets, through dimensional thread profiling, to ultimate tensile break testing.
We work directly from STEP, IGES, DXF files, or physical customer samples to turn custom designs into prototypes within 7 days, scaling smoothly to multi-thousand unit batch production runs for OEM brands.
Review your fastener drawings, custom anodizing specs, or batch volume quotes directly with our technical team. Export-ready compliance for UK & European engineering projects.